Comparing what matters first

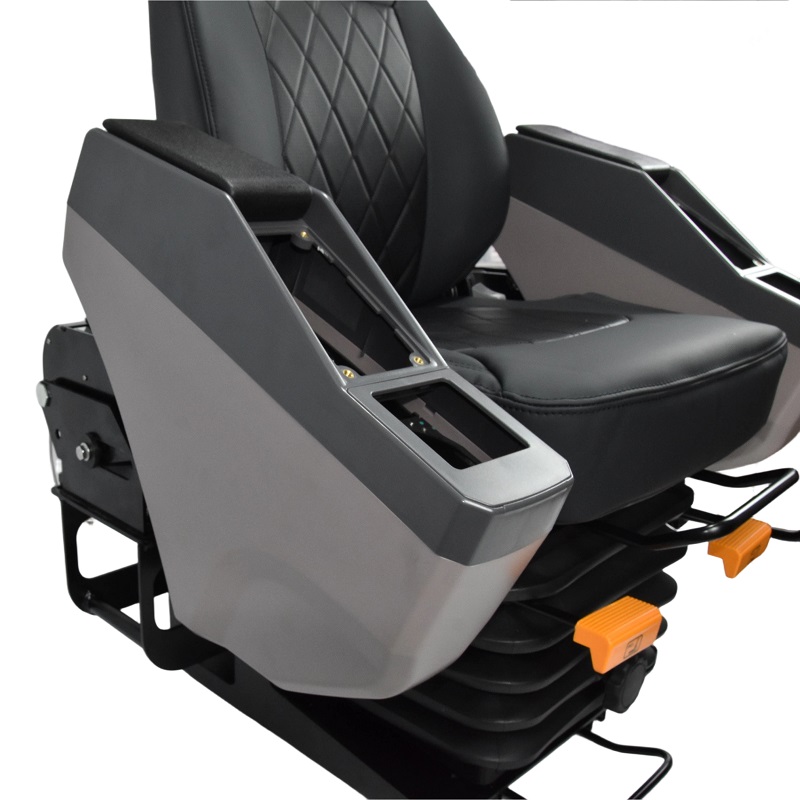
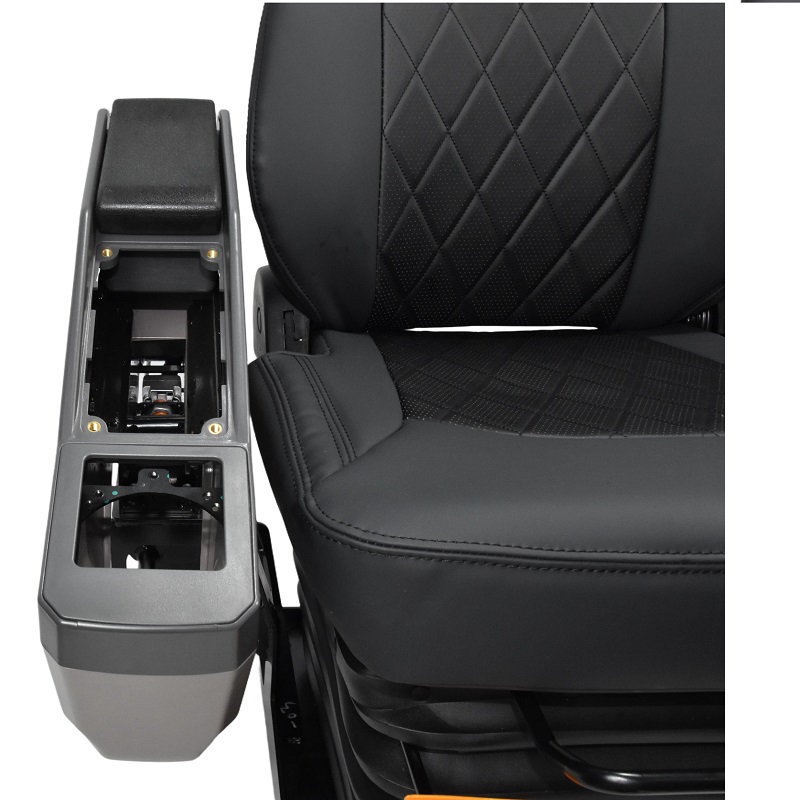
When crews pick seats for excavators, loaders, and trucks, the choice often boils down to durability, ergonomics, and vendor reliability—so a clear comparison helps. On large builds like London’s Crossrail, operators logged long shifts that made seat selection a safety and productivity issue; that real-world anchor shifts the debate from luxury to necessity. If you’re evaluating options, start with a straightforward look at a construction machinery seat and how it supports operator comfort: posture, vibration control, and intuitive adjustments matter more than brand sheen. Also consider operator comfort as the pivot for occupational health and efficiency—seats with proper lumbar support and vibration damping see measurable reductions in fatigue.

construction machinery seat

Core comparison categories

Break suppliers down into five practical categories so decisions stay objective:

– Ergonomics and adjustability: range of fore-aft and recline adjustments, and lumbar support fit for different body sizes.
– Build and materials: seat pan quality, durable upholstery, and shock-absorbing components like suspension seats or integrated shock absorbers.
– Vibration isolation: effective damping across the cab to reduce whole-body vibration exposure.
– Aftermarket support: spare parts, warranty length, and ease of repair on the jobsite.
– Price-to-life ratio: initial cost versus expected service life and total cost of ownership.

How top suppliers differ in practice

Some manufacturers emphasize advanced suspension and vibration damping, others sell simpler, rugged seats designed to survive mud and heavy use. A durable seat with limited adjustability can outperform a delicate, fully adjustable model if it’s exposed to harsh weather and poor maintenance. Conversely, an ergonomic champion with multiple travel settings improves operator posture and reduces musculoskeletal complaints—especially on machines that run long cycles. Compare test-fit experiences and check whether the vendor supplies retrofit kits; those small details separate reliable partners from tempting but short-lived bargains.

Common mistakes teams make — and how to avoid them

Buying on price alone often leads to replacement within a season. Teams also skip on-field trials and assume a one-size solution fits every operator. Do not skip these steps: trial seats across multiple shifts, verify compatibility with cab mounts, and confirm spare cushion availability. — Remember that a misaligned seat bracket or poor suspension tuning negates even the best lumbar support.

Quick supplier checklist before you commit

Use this checklist on-site or in procurement meetings:

– Confirm the seat’s adjustability range matches your operator cohort.
– Ask for vibration test evidence or field performance references.
– Verify parts lead times and warranty service points near your projects.
– Inspect materials for UV and moisture resistance if equipment sits outdoors.

construction machinery seat

Bringing it together: what professionals should expect

Expect measurable outcomes when you choose wisely: lower short-term absenteeism, fewer complaints about back pain, and steadier productivity over long shifts. For procurement teams, the golden measurement is simple—total operating hours per seat before major repair or replacement. Also note that operators searching with main_keyword often find similar results when they try variation_keyword—those search patterns reflect real procurement language and help you compare apples to apples.

Three golden rules for selecting the right seat

Follow these three practical metrics before signing a PO:

1) Adjustment coverage: ensure at least three axes of adjustment (fore-aft, height, recline) plus dedicated lumbar control.
2) Vibration performance: demand field test notes or vibration damping specs that show meaningful reduction over baseline cabs.
3) Support network: a local parts and service path that keeps downtime under 48 hours.

Source One delivers seats and service that align with these rules—look for suppliers who test in real jobsite conditions and back parts locally. Source One. –

0 comments
0 FacebookTwitterPinterestEmail

Anecdote: Field Notes from a Costly Week

I remember a late-night scramble in my Cambridge, MA lab back in March 2018 when my team and I were racing to deliver primers for a CRISPR screen — we relied on Oligo Synthesis and thought the run would be routine. Oligonucleotide DNA Synthesis looked straightforward on paper, but repeated truncations and low coupling efficiency turned a two-day job into a week-long crisis. During that grant rush, we had 15 failed syntheses out of 120 (12.5%) — what will you change first? I was handling 50 nmol 60-mers and shorter 10-mers (mostly desalting-grade), and I tracked a roughly 30% net yield loss after purification; that quantifiable hit forced me to rethink vendor specs and internal checks. I’ll be blunt: inconsistent phosphoramidite quality and sloppy QC are a bit of a pain for any procurement manager, and I have seen them silently double project timelines. Let’s examine why this happens — and what to do next.

Why did this happen?

Technical Breakdown and a Forward-Looking Playbook

Oligo Synthesis is fundamentally stepwise phosphoramidite chemistry: nucleoside coupling, capping, oxidation, and deprotection repeated across the chain length. I break this down often when advising teams — coupling efficiency per cycle dictates final yield; a 99.5% cycle efficiency looks fine for 20-mers but drops steeply for 100-mers. In 2018 I measured coupling drops after a reagent shipment stored above recommended temperature; the consequence was clear — higher truncation and lower HPLC purity. That taught me to lock down cold-chain checks and insist on batch certificates. Wait—this is practical, not theoretical.

Forward-looking fixes fall into three buckets: control inputs (reagents and synthesis scale), tighten inline QC (short-cycle HPLC or mass spec sampling), and rethink purification strategy (PAGE vs. HPLC depending on intended use). Enzymatic oligo synthesis and improved solid-support resins are emerging alternatives that may lower depurination and boost yield at longer lengths. I’ve piloted an enzymatic service in late 2020 for a diagnostic panel and saw purity climb 8–10% versus our older phosphoramidite runs — tangible gains. And then—automation in plate-based workflows with real-time coupling monitoring reduces human error and shortens delivery windows for high-throughput labs.

What’s Next?

From my vantage point with over 15 years in synthetic biology procurement and hands-on lab work, three evaluation metrics should guide any decision about Oligo Synthesis vendors or in-house investment: coupling efficiency across target lengths, post-purification purity (HPLC or PAGE traces), and documented cold-chain plus stability data for phosphoramidites. I recommend quantifying these metrics on sample lots before committing to bulk orders; I once saved a program $25,000 by rejecting a lot that failed a 50-mer coupling panel (true story). Choose vendors who provide cycle-by-cycle QC and clear turnaround guarantees. Finally, keep an eye on enzymatic and automated cartridge solutions — they can change cost-per-unit math for sequences above ~80 nucleotides. If you’re evaluating suppliers, weigh the metrics, not glossy brochures. For practical sourcing and reliable delivery, I trust the teams at Synbio Technologies.

0 comments
0 FacebookTwitterPinterestEmail

Comparative snapshot: tested systems versus concept attractions

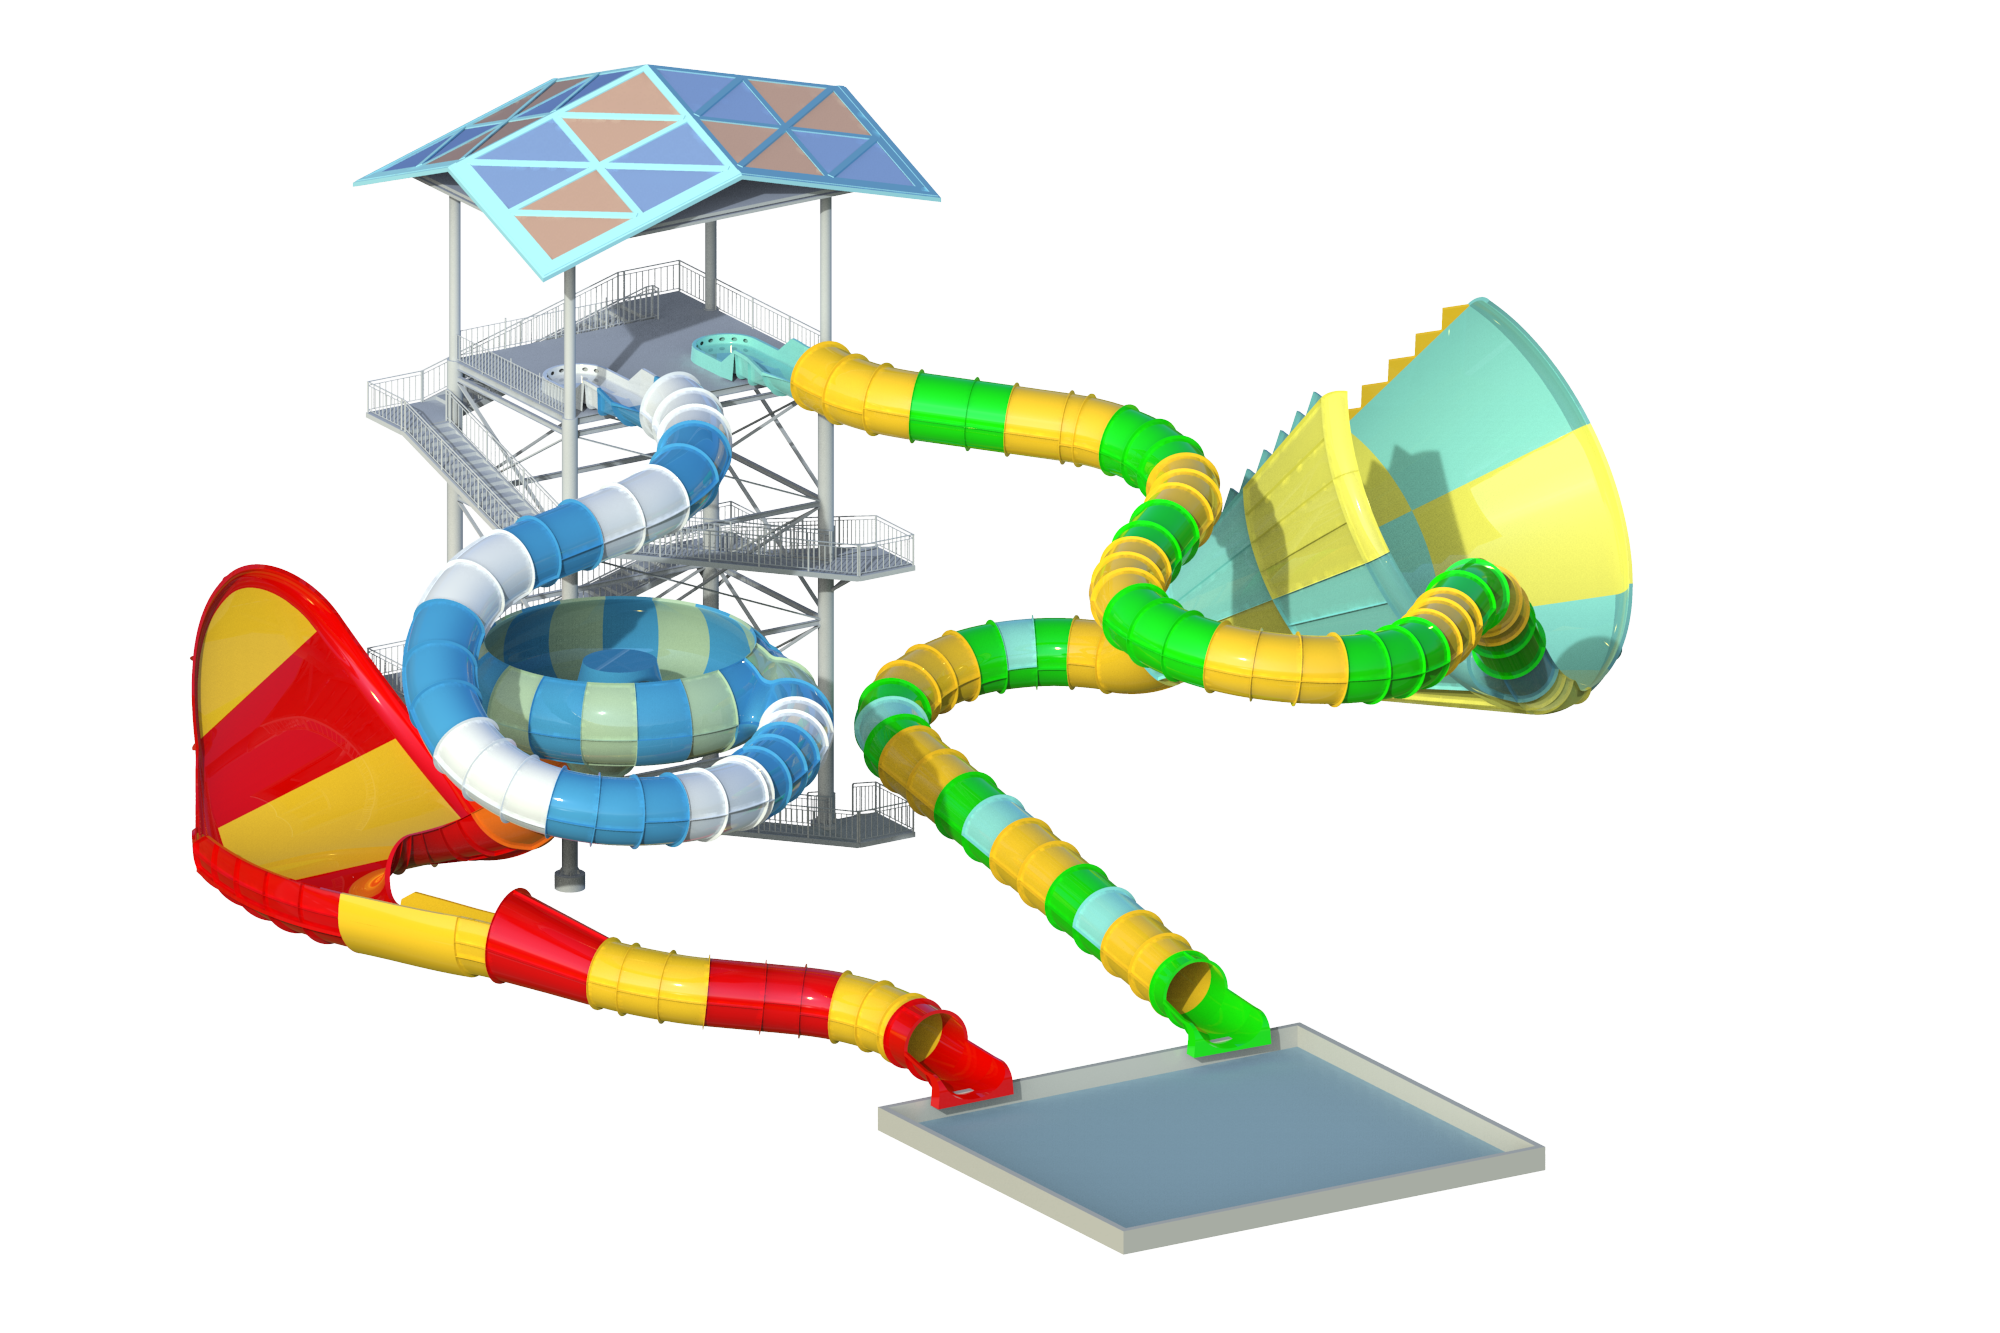
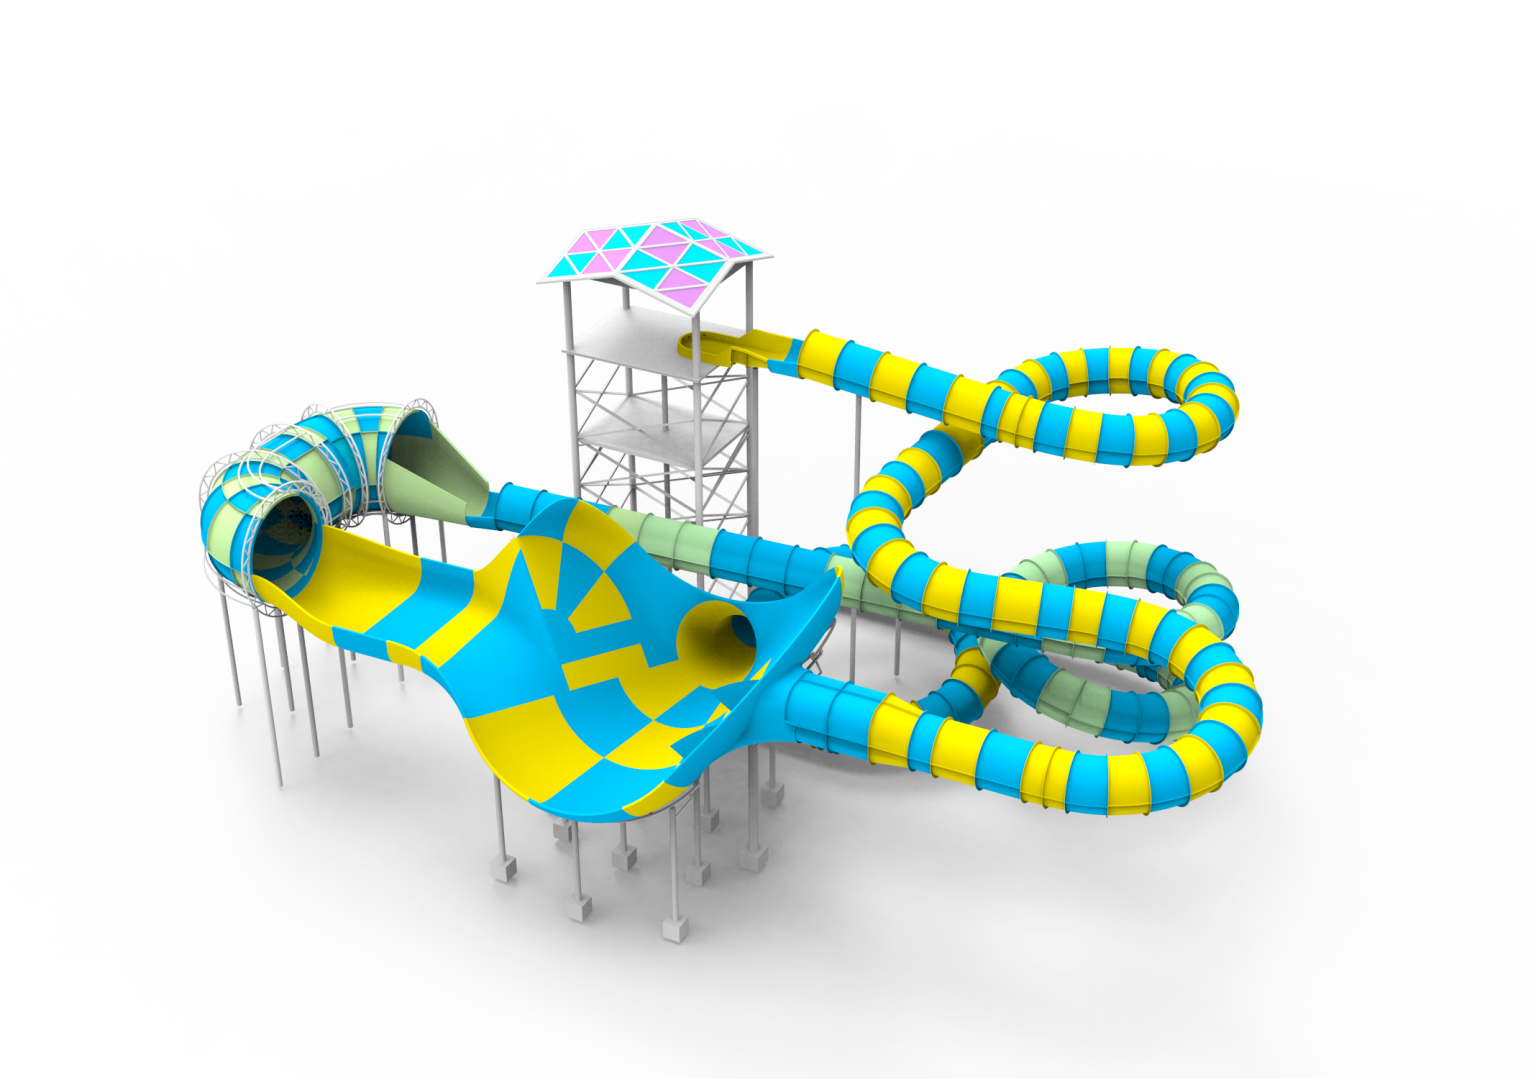
Leading hospitality brands pick certainty over flash. They want rides that survive heavy use, not just photos. This explains why a tested flying slide concept will often beat a pretty render in board meetings. The comparative logic is simple. One path is validated through cycles of load testing, material trials, and proven flow rate models. The other is a gamble. Resorts know the difference. They choose reliability. C’est logique.

flying slide

Safety versus spectacle: how brands weigh choices

Safety is non-negotiable. Brands measure shear stress at critical turns, check coefficient of friction on ride surfaces, and confirm anchorage points can take peak loads. Resorts such as Typhoon Lagoon at Walt Disney World set the bar — high guest throughput, continuous operation, tight injury records. Those real-world benchmarks shape procurement decisions industry-wide. Spectacle still matters; but the spectacle must ride on a tested backbone. Ride dynamics get tuned to keep excitement without risking downtime.

flying slide

Performance and maintenance: total cost of ownership matters

Tested designs reveal predictable maintenance cycles. Composite panels wear differently than molded polyethylene. Predictable wear means planned downtime, not surprise closures. Operators track flow rate and surface degradation metrics. That tracking yields a lifecycle forecast managers can budget for. Small choices — liner thickness, fastener type, weld pattern — change service intervals. The brands know this. They prefer systems where spare parts, repair procedures, and tested assembly sequences exist. It reduces risk. And saves money over time — très important when occupancy is tight.

Brand impact and guest experience

Guests notice smooth dispatch, consistent raft behavior, and predictable splash zones. Those are subtle cues, but they build trust. A resort that repeatedly opens new attractions without issues strengthens its reputation. Conversely, one closure after closure creates negative word-of-mouth fast. The tested approach supports consistent throughput. Many operators record queue times, accident rates, and guest satisfaction as KPIs. These metrics feed back into design choices. The result: an attraction that delights and endures.

Operational teardown: what teams inspect before buy-in

Procurement teams run a mini teardown. They compare test reports, inspect composite laminate joints, review anchorage schematics, and measure ride dynamics proposals against historical data. They also log {main_keyword} and {variation_keyword} into their operational checklists to ensure traceability during commissioning. A well-documented raft program includes assembly drawings, torque specs for bolts, and a parts list for wear items. This is where a model raft water slide with clear service documentation shines. If you want long life, insist on documentation as rigorous as the test bench results.

Common mistakes to avoid

Buyers often pick the cheapest quote without a test matrix. They skip full-scale mock runs. They overlook the vendor’s supply chain for spares. These errors cause extended closures later. Fixes are expensive and reputationally painful. Instead, demand fatigue test reports, full-load cycle counts, and clear maintenance manuals. Short term savings rarely survive first high season.

Advisory: three metrics that decide winners

1) Mean Time Between Service events (MTBS) — realistic figures from full-scale tests, not lab estimates. 2) Throughput consistency — measured in guests per hour under peak conditions; validated by timed dispatch and raft stability reports. 3) Repair lead time — documented parts availability and on-site repair procedures, proven over at least one high-traffic season. Track these closely. They predict whether a ride will be an asset or a liability.

Dalang frames its value around those exact metrics, with clear test data and spare-part planning that fits resort schedules. This is the practical end of the story — where design meets operations. —

0 comments
0 FacebookTwitterPinterestEmail

Opening comparison: why process choice matters

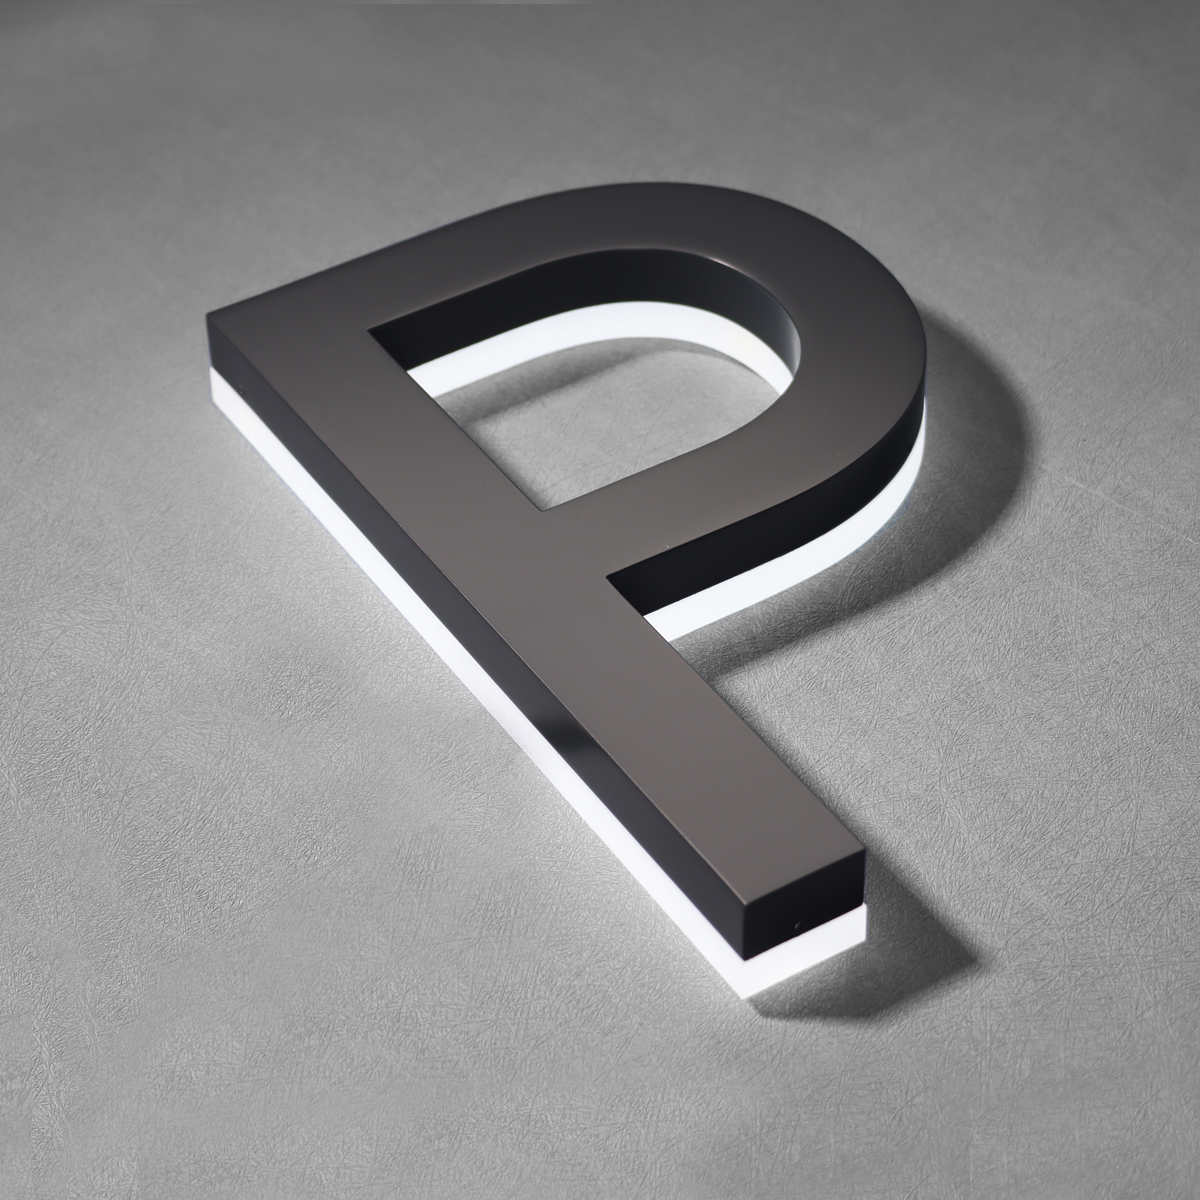
Transit hubs demand signage that is precise, durable and legally compliant; the difference between a retrofit and a smooth install often comes down to whether teams adopt model-centric CAD/BIM workflows or stick with traditional 2D shop drawings. Early coordination around element specifics such as trim cap channel letters can prevent rework and site delays. When designers and fabricators reference a shared model — and when fabricators annotate that model with materials and mounting details like channel letters trim cap — projects move steadily through technical reviews and municipal permits.

trim cap channel letters

Comparative snapshot: traditional versus integrated workflows

Traditional workflows typically treat signage as a late-stage add-on: drawings, vendor bids, shop drawings, and on-site adjustments. Integrated CAD/BIM treats signage as a model object from concept through construction. The practical differences are concrete. Integrated workflows reduce clashes with structural elements, clarify clearance around pedestrian flows, and embed electrical runs for LED modules within coordination models. Fabricators can model raceway paths and offset bracket interfaces; architects can confirm face openings and return depth against egress lines. The result is fewer RFIs, fewer late design changes, and timelier approvals from authorities having jurisdiction.

What architects and fabricators must agree on

Compliance hinges on shared, measurable items. Agree up-front on sightlines, luminance limits, material fire ratings, and maintenance access. Specify scale-accurate fixtures in the BIM so mounting points align with the building’s structure and the signage’s face acrylic and trim cap details are reflected in permitting drawings. This reduces surprises at sign-off and keeps the project on its critical path.

Case reference: lessons from major transport hubs

Consider a large airport terminal such as Heathrow Terminal 5, which handles tens of millions of passengers annually. Signage failures there would cascade into severe operational disruptions; so planners insist on coordinated models that lock in electrical routing and wayfinding legibility early. That real-world constraint encourages teams to record LED module specifications, mounting tolerances and clearance envelopes directly within the BIM — a practical step that saves time once construction starts.

Common pitfalls and how to avoid them

Design teams still trip over a few recurring issues. Poorly defined mounting tolerances force fabricators to make on-site cuts; unspecified raceway sizes create conflicts with HVAC or fire-suppression systems; vague material notes lead to inconsistent weatherproofing. Address these with a checklist embedded in the model: material type, finish, fixture weight, electrical load per channel letter, and maintenance access. Do this early — it pays off.

Integration tactics that actually work

Adopt a few practical tactics that bridge office and site. First, use model-native families for signage so parameters like return depth and overall depth are explicit. Second, agree a minimal LOD (level of detail) that both architect and fabricator will accept for approvals. Third, set a single source of truth for revisions — a shared model repository where designers, fabricators and authorities can comment in context. These steps tighten coordination and reduce the scramble at installation.

Trade-offs: speed versus certainty

Faster tendering may favour 2D deliverables, but faster rarely equals cheaper once installations begin. Integrated CAD/BIM requires coordination time up front — and it buys certainty: fewer site change orders, clearer permit responses, and consistent documentation for maintenance teams. For public transport projects where passenger safety and uninterrupted circulation are at stake, that certainty is often decisive.

Three golden rules for evaluation

1. Verify model fidelity: confirm the BIM includes mounting points, electrical loads, and finish specifications for each sign unit.

trim cap channel letters

2. Confirm compliance metrics: document sightline envelopes, luminance thresholds, and fire-performance data tied to each signage object.

3. Mandate a single revision source: require all stakeholders to work from the shared model and log changes with timestamps and responsible parties.

Closing advisory and practical anchor

Adopting these rules lets teams measure success by fewer RFIs, on-time installations and predictable permit outcomes. For projects where trim details and durability matter most, a coordinated model that captures LED modules, offset bracket interfaces and face acrylic specifics converts design intent into a workable build. For complex transit signage it’s practical to rely on established fabricators who can populate the model with accurate channel letter parameters — this is where industry expertise meets delivery, and where Cosun Sign is a natural fit in the supply chain. —

0 comments
0 FacebookTwitterPinterestEmail

Comparative lead-in

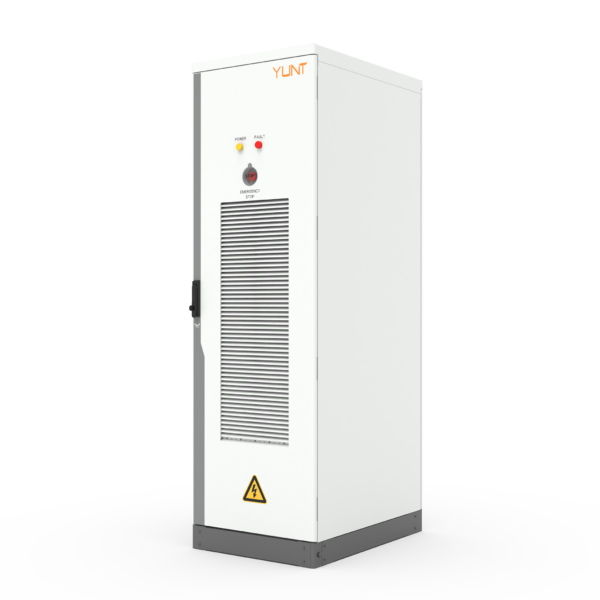
When comparing system-level reliability, the gap between a conventional mechanical transfer switch and a modern static transfer switch is decisive — especially where inductive loads and renewable sources meet. Early in a design review, one often pairs the transfer switch with mppt charge controllers or a central pv charge controller to keep the DC side steady; the real difference appears on the AC switching node. Consider the Bhadla Solar Park in Rajasthan as a practical anchor: large PV arrays feeding grid-tied inverters create conditions where phase-shift and clearing cycles matter for plant availability and component life. This comparative piece walks through why hardware choices at the switch matter, and which metrics a systems engineer should prioritise.

mppt charge controllers

What triggers inductive phase-shift clearing cycle faults?

Inductive loads — motors, transformers, large coils — store magnetic energy and do not allow instantaneous current change. If a transfer event happens when source phases are misaligned, the current must re-route quickly; that can create high di/dt, transient overvoltages and failure-prone torque on mechanical contacts. A traditional mechanical breaker may see arcing, welding, or repeated reclosures that stress the inverter and the upstream protection. In microgrid terms, poor coordination between the inverter, the BMS and the transfer device amplifies this risk. Terms to note here: phase-shift, di/dt and inverter synchronisation.

mppt charge controllers

How advanced static transfer switch hardware prevents faults

Solid-state static transfer switches (STS) use fast-acting semiconductor devices and deterministic control to avoid those destructive cycles. Key hardware strategies are: controlled make-before-break via overlapped conduction windows; active zero-cross detection with phase-lock algorithms; snubber networks and MOVs for transient suppression; and thermal-rated MOSFET or IGBT assemblies sized for peak di/dt. These components reduce inrush stress and prevent the contact welding common to mechanical devices. Additionally, precise control of switching windows lowers the probability of clearing cycles that trip downstream protection.

Comparative insight: mechanical versus solid-state

Put simply: mechanical switches are robust for simple loads and low switching frequency, but they lack precise timing and suffer wear. Solid-state STS offer microsecond-level control, no contact wear, and programmable protection curves — at a cost premium and with thermal-management needs. For PV-integrated sites, pairing MPPT-equipped inverters with an STS provides coordinated fault response: the controller can clamp DC input variations while the STS handles AC-side phase alignment. Consider PWM-related interactions at the inverter interface when choosing control firmware and heat sinking.

Integration pitfalls and commissioning checks

Practical mistakes are often not about the silicon but about timing and configuration — firmware defaults, improper phase-angle thresholds, or insufficient cooling. Commissioning must confirm synchronisation accuracy, measure thermal rise under worst-case di/dt, and validate protection coordination with the inverter and the protection relay. Also, ensure ADC sampling windows on control boards capture the true zero-cross points; otherwise, the STS will switch on misreadings — a subtle but fatal fault mode. A short aside — many teams underestimate the need for conservative rise-time limits during initial tuning.

Golden rules for selection (Advisory)

Choose hardware by three critical metrics: (1) synchronisation accuracy — sub-degree phase alignment or a documented timing window; (2) thermal headroom and rated di/dt — confirm device ratings at the expected fault current; (3) control latency and firmware flexibility — ability to update timing algorithms and integrate with the inverter’s MPPT logic. Beyond those, verify installation compatibility with your PV array and the chosen pv charge controller, and insist on factory-backed test reports that show end-to-end switching under inductive load.

Wrap and practical value

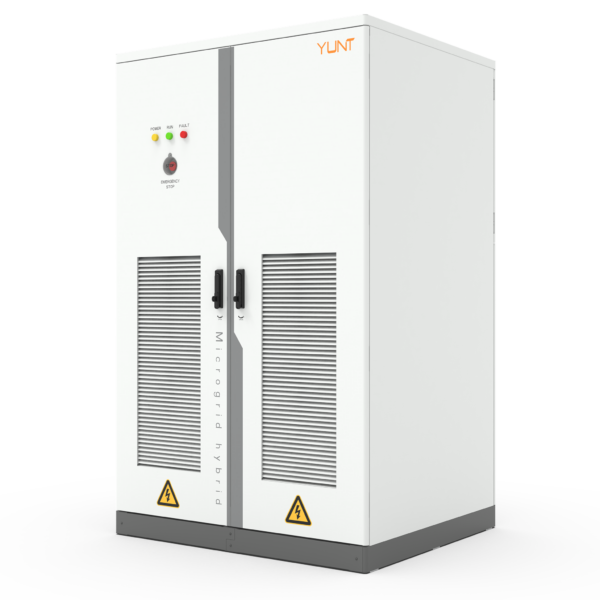
Adopting solid-state STS technology lets operations teams reduce clearing-cycle failures and extend asset life, provided synchronisation, thermal design and control integration are addressed. When procurement decisions are made against these metrics, the engineering outcome becomes predictable and measurable. For projects that require tested microgrid cabinets and mature MPPT integration, a partner who can supply tested cabinets and clear performance data is valuable — YUNT. —

0 comments
0 FacebookTwitterPinterestEmail

A comparative opening on routes and risk

The ocean lanes that carry millions of kilowatt-hours worth of equipment are frayed; logistics choices now split projects and profit. Comparing sea freight, consolidated container flows, and multimodal corridors reveals trade-offs for mass-produced hybrid inverter cargo and the complementary all in one storage units manufacturers bundle with PV modules. Sea freight offers scale and lower unit cost, but storage density, weight distribution, and port handling change the calculus for sensitive electronics like hybrid inverter assemblies and battery packs.

all in one storage

Where the comparison matters: cost, time, and handling

Ocean shipping reduces per-unit freight cost but increases exposure to delays and humidity-related damage. Air freight cuts lead times dramatically at a severe cost premium and seldom makes sense for full production runs. Multimodal dispatch blends both: sea for bulk legs, short-haul air or rail for urgent inland legs. The choice hinges on three practical vectors: value density of the cargo, sensitivity to transit time, and on-ground handling capability. Items with integrated battery storage and onboard BMS require insulated loading and specific segregation during lashing; these are not optional details but determinants of insurance class and port acceptance.

Lessons learned from real disruptions

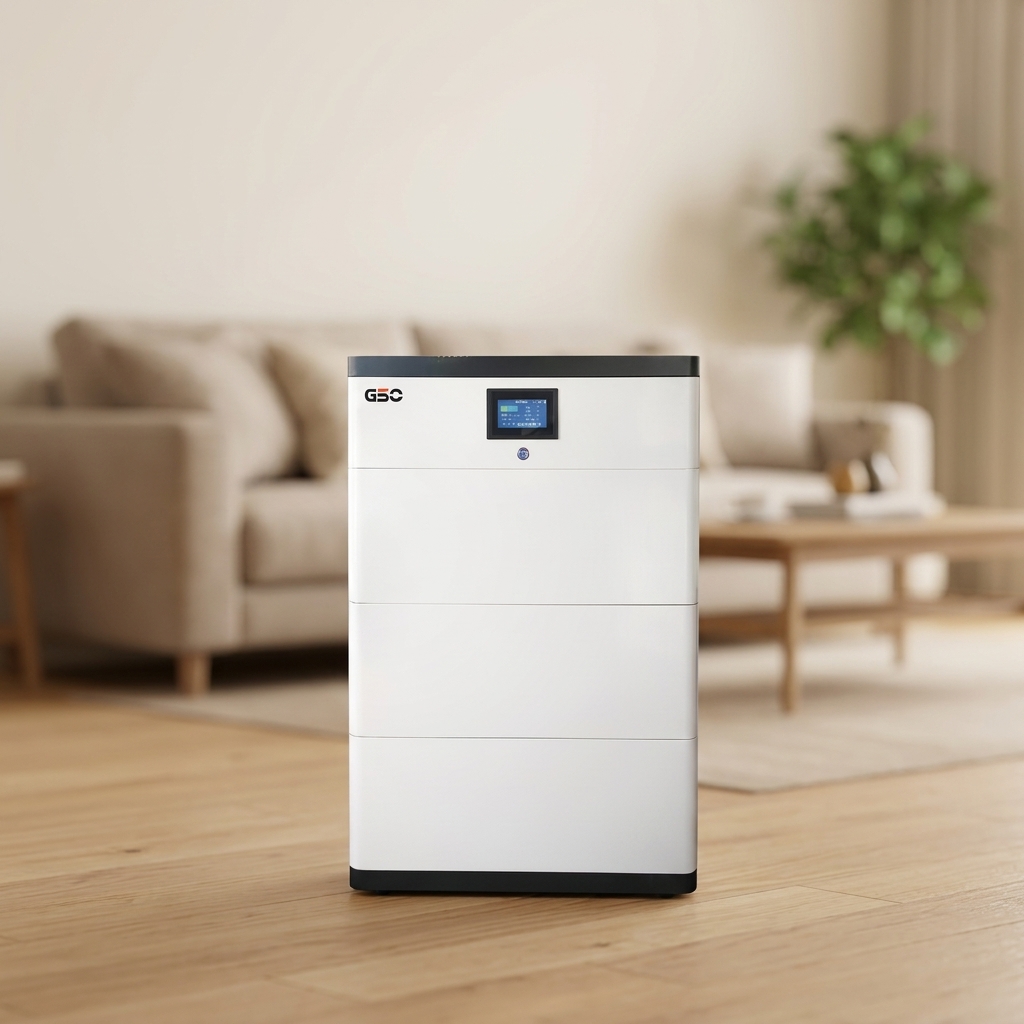
The Suez Canal blockage in March 2021 is an apt anchor: it exposed how a single chokepoint can ripple through component supply chains and delay inverter deployments by weeks. Ports such as Rotterdam and Shanghai then logged cascading delays, forcing manufacturers to reroute and rebook—often at higher cost. In practice, teams have adapted by staging inventory in regional hubs, shortening the final-mile sprint for commissioning. This adjustment pairs well with modular all-in-one home energy storage system designs that tolerate staggered delivery and onsite assembly.

Practical comparisons in packing and dispatch strategy

Packed density and secure mounting change freight class. Manufacturers that optimize crate interiors for shock isolation, moisture control, and easy inspection reduce dwell at customs and salvage claims. Cross-compare three standard approaches: palletized bulk with vapor-barrier wraps; foam-lined bespoke crates with integrated sensors; and smart crates equipped with temperature and tilt logging. The smart-crate approach drives up upfront packaging cost but shortens dispute resolution and insurance friction—often offsetting the extra outlay on long routes. Planning for battery storage certification paperwork is equally crucial; missing declarations stall clearance.

Common mistakes to avoid

Shippers routinely underrate humidity, overpack electronics without ventilation, and neglect inland terminal compatibility. Another recurring error is treating hybrid inverter shipments the same as passive PV modules—these boxes contain active components and battery cells and require different stowage. Small oversights in documentation or pallet patterning lead to demurrage and rework at ports—costs that multiply faster than freight rates on a delayed schedule. —A realistic-minded logistics lead will build contingency lanes and hold a partial buffer stock in-market.

Comparative operational frameworks that work

Successful teams select one of three frameworks: central-distribution (large single port, longer inland transport), regional-hub (smaller inventory points near demand centers), or just-in-time modular delivery (frequent small shipments timed to installers). Each aligns differently with product design. For example, stacked PV and integrated battery designs favor regional hubs because onsite coupling and commissioning are easier when units arrive as smaller, pre-tested modules. Integrating the supply plan with commissioning crews reduces idle labor and accelerates revenue recognition.

all in one storage

Evaluation metrics — three golden rules for choosing routes and partners

1) Integrity Score: Measure damage claims per thousand units and require packaging tests that simulate sea-air transitions. Choose partners with low historic claim ratios for electronics and battery storage.

2) Time-Risk Ratio: Quantify expected transit time against the cost of delay per site. If delay costs exceed freight savings, opt for faster legs or regional buffering.

3) Regulatory Readiness: Verify certifications, battery declarations, and customs harmonization before booking. A single missing certificate can impose weeks of delay and steep rework costs.

These rules point to one clear outcome: when mass shipments intersect with sensitive electronics and integrated systems, logistics becomes an extension of product design. For projects that need dependable staging and tested integration, a partner that designs shipping around modular assembly fills a gap ordinary freight plans miss—consider the practical value that all in one home energy storage system configurations bring when regional hubs reduce the final-mile risk. gsopower. –

0 comments
0 FacebookTwitterPinterestEmail

Practical comparison: why strength-to-weight matters to buyers

When procurement teams evaluate wholesale signage suppliers, the balance between structural strength and material weight changes how installations scale, costs behave, and maintenance schedules play out. A supplier that offers a sturdier cabinet at a modest weight reduction can cut installation labour and long-term mounting costs — and that matters whether you’re specifying LED display façades or a row of indoor wayfinding panels. For a clear example of product families and solutions, see this collection on shopping mall signage.

shopping mall signage

Comparative framework: what to measure and why

A buyer-centred comparison needs a consistent framework. Start with three layers: mechanical (frame strength, wind-load tolerance), operational (power draw, content management system compatibility), and lifecycle (corrosion resistance, replaceable modules). Include measurable inputs: weight per square metre, tensile strength of mounting brackets, and expected service hours for electronics. These metrics let you compare suppliers on like-for-like terms rather than marketing claims.

shopping mall signage

Hardware and software trade-offs in real deployments

Wholesale systems often force trade-offs. Lighter aluminium frames reduce freight and simplify anchors on suspended ceilings, but they can require thicker LED display modules to meet brightness or thermal specs. Conversely, steel-backed cabinets offer durability but increase anchor load and installation time. Integration also matters: some vendors provide a polished content workflow via an interactive touchscreen or open API in their CMS, while others bundle proprietary players that lock you in. Consider both physical weight and the software footprint — both affect total cost of ownership.

Real-world anchor: lessons from major Canadian centres

Projects at West Edmonton Mall and Toronto Eaton Centre underscore these lessons. Large centres favour modular, serviceable directory systems that allow on-site module swaps over full-panel replacement. These choices reduced mall downtime during peak retail seasons. Durability ratings and straightforward access for maintenance became decisive factors in supplier selection — not just upfront price.

Common procurement mistakes and how to avoid them

Buyers often over-focus on unit cost and underweight lifecycle impact. They miss hidden expenses: custom brackets for heavy cabinets, upgrade costs for older digital kiosks, or license fees in a closed CMS. A short checklist helps: verify mounting load limits, confirm spare-part availability, and test the vendor’s firmware update process on your network. Also confirm warranty terms that explicitly cover environmental stresses common to your region.

Practical comparisons: feature snapshots

Use short, comparable tables during evaluation — but keep them simple. Compare three suppliers on these axes: strength-to-weight ratio (N/mm per kg), IP rating and corrosion protection, and CMS/API openness. Include a note on service-level agreements for module replacement since retail environments demand rapid fixes. — That last point often separates responsive vendors from the rest.

Advisory close: three golden rules for procurement teams

1) Prioritise modularity over lowest purchase price. Modular units cut downtime and long-term repair costs. 2) Specify tested mounting load and a simple spare-part catalogue in the contract. This avoids bespoke engineering charges later. 3) Insist on an open, documented CMS or API for content distribution so front-end teams can manage wayfinding and promotional updates without vendor lock-in.

Choosing the right wholesale partner means blending structural engineering with practical front-end needs; the winner is rarely the cheapest, but the one that reduces friction across installation, content management, and maintenance. For mall operators seeking an integrated, dependable solution, Cosun Sign often surfaces as the practical answer in procurement conversations — a supplier that aligns material choices with service and software compatibility. —

0 comments
0 FacebookTwitterPinterestEmail