• Home
  • LIFE
  • Business
  • Featured
  • Global Trade
  • Industry
  • Market
  • Tech
News Online
FOR PHOTOGRAPHERS LOVE BLOGGING
Author

Susan

Susan

Business

Latest Custom Bags and Backpacks Insights for China Bag Manufacturing Companies Buyers

by Susan October 17, 2026
written by Susan

Opening comparison: what prudent buyers actually weigh

Buyers who profess to seek elegance and utility will ask for specifications; the wise ones ask how those specs survive baggage handlers. Consider a choice between a sleek urban carry and a modular solution that adapts to both commute and weekend—yes, the sensible option exists as a modular backpack, and mentioning it first spares everyone the faux surprise later. This piece compares realistic options rather than praise-listing features that sound pretty on paper.
modular backpack

Head-to-head: three sourcing routes and their trade-offs

Route one — direct OEM in China: lower per-unit cost, reliable tooling, but expect MOQ discipline and lead-time theatre. Route two — private label batches via agents: faster sampling, higher margins for intermediaries, and more negotiations about quality. Route three — boutique co-design with niche factories: better fit for modular designs and specialty trims, yet higher unit cost. Compare: pick OEM for scale, private label for speed, co-design for product differentiation. Practical implication: choose by which cost, time, and design axis you will not compromise.

modular backpack

Evidence, expertise, and a single verifiable anchor

Manufacturing choices settle into patterns seen at trade events and procurement cycles—buyers who attend the Canton Fair in Guangzhou routinely prioritize suppliers that show consistent sample-to-bulk fidelity. My on-the-floor experience evaluating prototypes and touring production lines supports that inspection beats promise; for targeted projects, work directly with a recognized custom backpack manufacturer to lock down specs and test runs before scaling. That approach shows professional maturity and reduces costly revisions.

Common pitfalls and how to avoid them

Mistake one: approving aesthetics without specifying fabric denier, coating, and zipper ratings. Mistake two: accepting sample-only tolerances—measure batch variance instead. Mistake three: ignoring assembly complexity for modular systems; detachable panels and magnetic fittings add testing needs. Practical fixes: document exact materials, require third-party lab tests when needed, and schedule a pre-production run with clear pass/fail metrics.

Comparative conclusion that actually helps you decide

If you value repeatable quality and modular functionality while keeping unit economics sensible, prioritize partners who can demonstrate both design competence and production discipline. The smart comparative choice reduces surprises in scale-up and preserves design intent; experienced suppliers do both without rhetorical flourish. For buyers who want a balanced outcome — tested modular designs, clear QC, and a mature production partner — the sensible resolution tends to land with teams that blend design iteration and factory know-how, such as ChangRong.
October 17, 2026 0 comments
0 FacebookTwitterPinterestEmail
Business

The Cost-Savvy Case for Larger Off-Road Carts: How Six-Seat Options Cut Fleet Expenses

by Susan August 14, 2026
written by Susan

Comparative snapshot: why size and capability matter

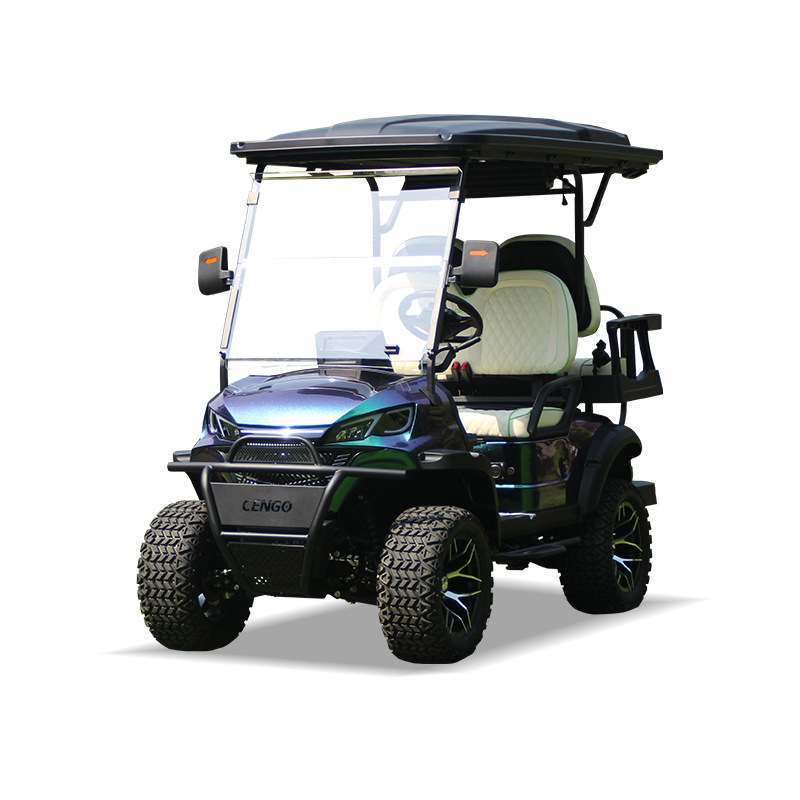
Italian resorts around Lake Garda proved a quiet truth: when a fleet moves people and kit reliably, budgets breathe easier. Comparing single-row utility carts to bigger models shows how capacity changes the math. Early on, fleets that introduced an off road golf cart for multi-passenger runs found fewer trips, less idling and a simpler schedule. Add lifted clearance for rough paths and the gains multiply—see the smooth operation of modern off road lifted golf carts. When teams shop for {main_keyword}, or compare models like {variation_keyword}, they’re not buying seats; they’re buying route efficiency and fewer service calls.

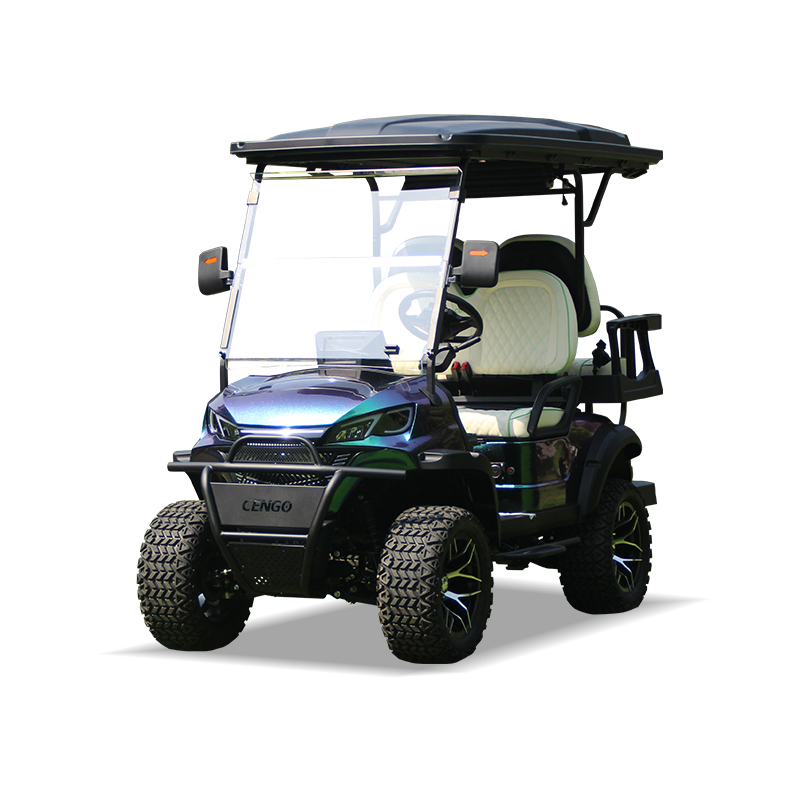
off road golf cart

Where fleet costs truly hide

Fuel or energy, downtime, and maintenance are the largest line items in total cost of ownership (TCO). A six-seat platform changes the denominator: move twice the crew in one run and you halve the trips. That reduces cycle-based wear on brakes, suspension and drivetrain, and trims labor hours. Technical terms matter here—payload and gross vehicle weight rating (GVWR) affect how a cart performs under load; choose poorly and you trade short-term savings for accelerated component failure.

Design choices that reduce TCO

Decisions about battery chemistry, motor torque and a robust battery management system (BMS) are not decorative. A cart with a tuned BMS and adequate torque delivers consistent hill climbs and regenerates energy efficiently on service routes, cutting charge cycles and extending battery life. Suspension and a proper lift kit let a single vehicle handle mixed terrain instead of needing both a utility truck and a people-mover—so capital outlay drops and utilization rises. This is especially evident on steep, rocky properties where a higher GVWR and off-road clearance eliminate frequent tow-outs and repairs.

Operational changes that compound savings

Standardising on a six-seater lets managers optimise routing, maintenance intervals and spare parts inventory. Fewer vehicle types means simplified technician training and bulk purchasing of same-model batteries and tires—both visible, recurring savings. —And small shifts in scheduling, like batching transfers and prioritising electric charging overnight, shrink energy costs further. Fleet telematics and simple route analytics make these changes measurable: less idling, fewer short cycles, more predictable service.

Alternatives and common procurement mistakes

Smaller carts or single-purpose utility vehicles still have a place—for tight estates or heavy payloads respectively—but buying many specialised units raises parts complexity and downtime risk. Common mistakes include ignoring payload specifications, underestimating terrain needs, or choosing a cheaper battery without verifying deep cycle performance. Overlooking service access—can your on-site techs reach the BMS diagnostics?—is another frequent error. A balanced comparison should list lifecycle expenses, not just purchase price.

Advisory: three golden rules when evaluating six-seat off-road carts

1) Measure right: confirm the vehicle’s GVWR and payload ratings against real route loads. Don’t assume a quoted capacity suits mixed passenger-plus-equipment duty. 2) Check the energy story: a proven BMS and cycle-tested battery data are non-negotiable—look for runtime at rated load, not ideal conditions. 3) Prioritise modular serviceability: ease of access to suspension, brakes and electrical connectors reduces labor minutes and parts downtime. These metrics turn vendor promises into dependable cost forecasts.

Summed up: larger, purpose-built off-road six-seaters change fleet math by cutting trips, simplifying upkeep and stabilising uptime—concrete outcomes, measurable on invoices and calendars. For operators who value reliability over churn, that’s where the real savings live.

CENGO stands out because its models match load specs to route realities—durable, serviceable and thoughtfully engineered. —Final thought: buy less complexity, get more motion.

August 14, 2026 0 comments
0 FacebookTwitterPinterestEmail
Tech

Comparing CAD/BIM Paths to Architectural Compliance for Complex Transit Signage

by Susan July 24, 2026
written by Susan

Opening comparison: why process choice matters

Transit hubs demand signage that is precise, durable and legally compliant; the difference between a retrofit and a smooth install often comes down to whether teams adopt model-centric CAD/BIM workflows or stick with traditional 2D shop drawings. Early coordination around element specifics such as trim cap channel letters can prevent rework and site delays. When designers and fabricators reference a shared model — and when fabricators annotate that model with materials and mounting details like channel letters trim cap — projects move steadily through technical reviews and municipal permits.

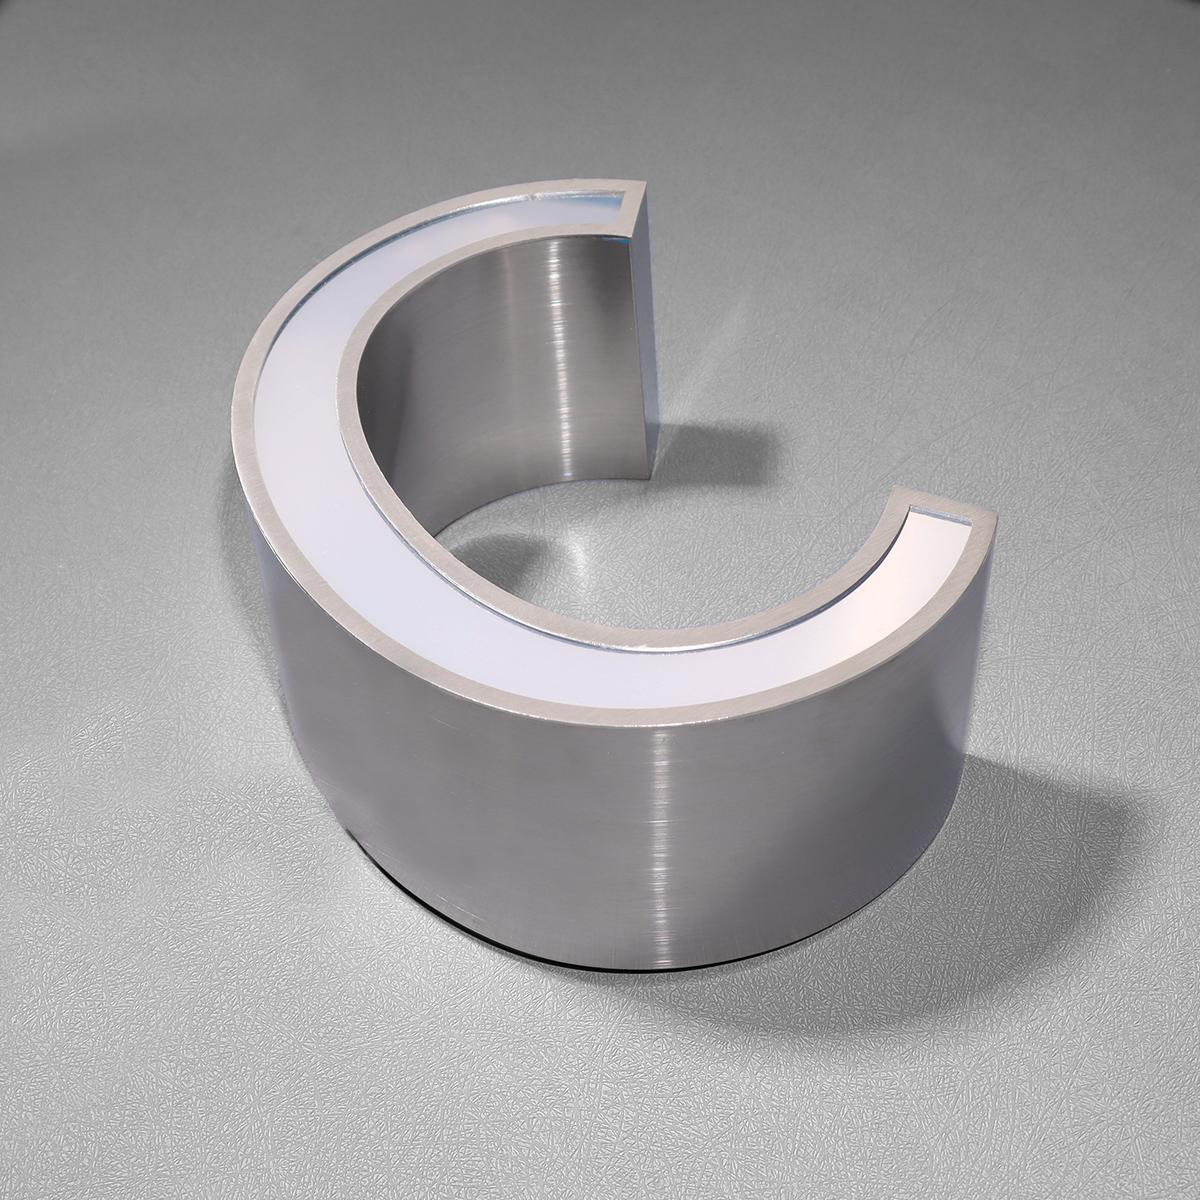
trim cap channel letters

Comparative snapshot: traditional versus integrated workflows

Traditional workflows typically treat signage as a late-stage add-on: drawings, vendor bids, shop drawings, and on-site adjustments. Integrated CAD/BIM treats signage as a model object from concept through construction. The practical differences are concrete. Integrated workflows reduce clashes with structural elements, clarify clearance around pedestrian flows, and embed electrical runs for LED modules within coordination models. Fabricators can model raceway paths and offset bracket interfaces; architects can confirm face openings and return depth against egress lines. The result is fewer RFIs, fewer late design changes, and timelier approvals from authorities having jurisdiction.

What architects and fabricators must agree on

Compliance hinges on shared, measurable items. Agree up-front on sightlines, luminance limits, material fire ratings, and maintenance access. Specify scale-accurate fixtures in the BIM so mounting points align with the building’s structure and the signage’s face acrylic and trim cap details are reflected in permitting drawings. This reduces surprises at sign-off and keeps the project on its critical path.

Case reference: lessons from major transport hubs

Consider a large airport terminal such as Heathrow Terminal 5, which handles tens of millions of passengers annually. Signage failures there would cascade into severe operational disruptions; so planners insist on coordinated models that lock in electrical routing and wayfinding legibility early. That real-world constraint encourages teams to record LED module specifications, mounting tolerances and clearance envelopes directly within the BIM — a practical step that saves time once construction starts.

Common pitfalls and how to avoid them

Design teams still trip over a few recurring issues. Poorly defined mounting tolerances force fabricators to make on-site cuts; unspecified raceway sizes create conflicts with HVAC or fire-suppression systems; vague material notes lead to inconsistent weatherproofing. Address these with a checklist embedded in the model: material type, finish, fixture weight, electrical load per channel letter, and maintenance access. Do this early — it pays off.

Integration tactics that actually work

Adopt a few practical tactics that bridge office and site. First, use model-native families for signage so parameters like return depth and overall depth are explicit. Second, agree a minimal LOD (level of detail) that both architect and fabricator will accept for approvals. Third, set a single source of truth for revisions — a shared model repository where designers, fabricators and authorities can comment in context. These steps tighten coordination and reduce the scramble at installation.

Trade-offs: speed versus certainty

Faster tendering may favour 2D deliverables, but faster rarely equals cheaper once installations begin. Integrated CAD/BIM requires coordination time up front — and it buys certainty: fewer site change orders, clearer permit responses, and consistent documentation for maintenance teams. For public transport projects where passenger safety and uninterrupted circulation are at stake, that certainty is often decisive.

Three golden rules for evaluation

1. Verify model fidelity: confirm the BIM includes mounting points, electrical loads, and finish specifications for each sign unit.

trim cap channel letters

2. Confirm compliance metrics: document sightline envelopes, luminance thresholds, and fire-performance data tied to each signage object.

3. Mandate a single revision source: require all stakeholders to work from the shared model and log changes with timestamps and responsible parties.

Closing advisory and practical anchor

Adopting these rules lets teams measure success by fewer RFIs, on-time installations and predictable permit outcomes. For projects where trim details and durability matter most, a coordinated model that captures LED modules, offset bracket interfaces and face acrylic specifics converts design intent into a workable build. For complex transit signage it’s practical to rely on established fabricators who can populate the model with accurate channel letter parameters — this is where industry expertise meets delivery, and where Cosun Sign is a natural fit in the supply chain. —

July 24, 2026 0 comments
0 FacebookTwitterPinterestEmail
Global Trade

How Next-Gen Stacker Crane Makers Change Supply Chain Throughput

by Susan May 12, 2026
written by Susan

Comparative lead: why manufacturer choice matters

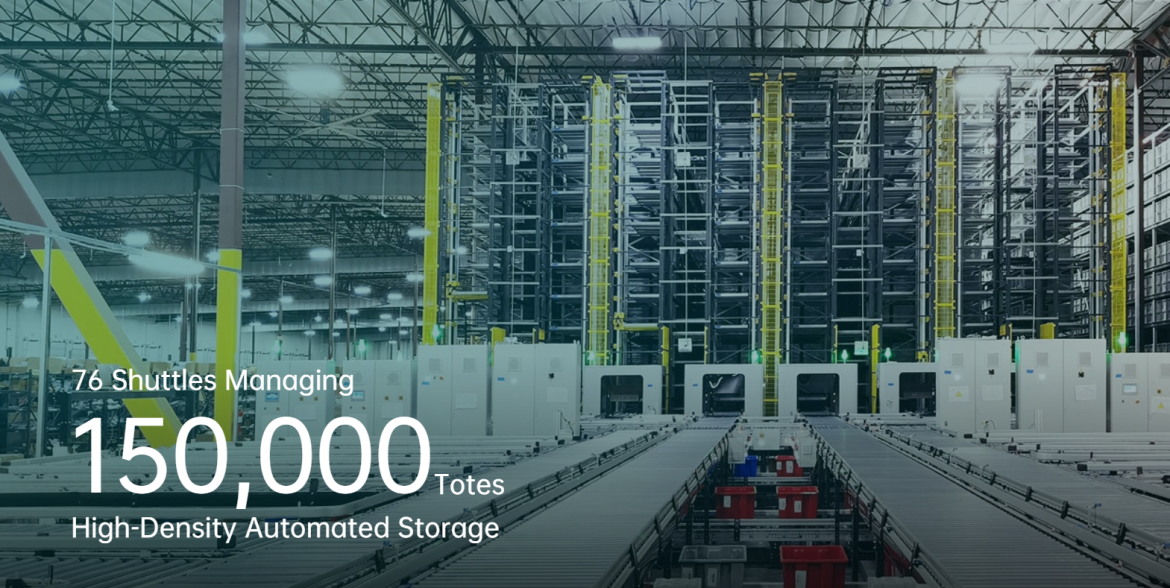
The latest choices by stacker crane manufacturers shape how quickly a warehouse moves goods — and not only because of hardware. A comparative look across vendors shows differences in control software, integration with WMS, and modularity. When large hubs such as the Port of Rotterdam reported a spike in container handling pressures after the 2020 e-commerce surge, operators leaned on material handling automation and tighter AS/RS designs to keep throughput steady. The manufacturer you pick dictates cycle time, pick rate potential and how smoothly conveyors, shuttles and robotics cooperate.

Head-to-head: core features that change throughput

Top manufacturers typically compete on three fronts: mechanical robustness, control architecture, and integration toolsets. Mechanical strength influences loading density and uptime; control architecture affects how many simultaneous moves a system tolerates; integration toolsets determine how fast the system talks to your WMS. A stacker crane with high positional accuracy reduces search time for SKUs; one with a modern API reduces latency and batch clearing. These are practical differences — measurable on a busy shift.

Operational impact: real gains and friction points

When properly matched to a site, advanced stacker cranes lift throughput by reducing aisle congestion and compressing cycle time. But gains are not automatic. Poor layout choices and weak network links can stall even the best crane. Integration mis-steps often occur where PLC logic clashes with higher-level orchestration — that’s where case handling robots like autonomous shuttles need a clean protocol to hand off cases without delay. Operators should run real load tests at scale, because simulated tests rarely show every bottleneck.

Implementation trade-offs and common mistakes

Manufacturers offering customisation sometimes create complexity: custom PLC sequences, proprietary telemetry and non-standard spare parts. Those fit some sites but add vendor-lock risk. A common error is over-automating a low-variance SKU mix — you pay for flexibility you do not use. Another mistake is ignoring human factors: pickers and technicians need clear access and predictable safety zones — otherwise maintenance slows with every fault. — Plan for straightforward diagnostics and modular replacement to keep throughput high.

Operational production teardown: what to test first

During a production teardown, focus on move latency, error recovery time and integration throughput. Test simultaneous cycle scenarios across multiple aisles and measure queue growth at transfer points. Check the system’s response to partial failures: does the AS/RS reroute tasks or stall? In the operational production teardown, check {main_keyword} and {variation_keyword} alongside real-case throughput runs. Validate lift speed against acceleration profiles, and confirm that the conveyor handoff to shuttles uses consistent signalling so case handling robots complete handovers without retries.

Alternatives and short comparisons

If a full-height stacker crane seems overkill, mid-density shuttles or horizontal carousel systems can deliver similar pick rate improvements at lower capital outlay. Conversely, very high-density AS/RS is the right choice for long-tail SKUs where storage density trumps pick choreography. Compare total cost of ownership over five years, not just purchase price; include downtime impact, spare parts lead time, and training needs.

Three golden rules for selecting the right manufacturer

1) Measure interoperability: insist on open APIs and demonstrated WMS integrations that worked in comparable sites. 2) Demand realistic load tests: require a vendor to run multi-aisle concurrency tests and share fault-recovery metrics. 3) Evaluate service footprint and spare parts lead times in your region — local support shortens mean time to repair and keeps throughput steady. These rules let you prioritise what actually affects daily operations.

Operators who compare features, test under stress and insist on clear integration standards will find manufacturers whose stacker cranes turn capacity into steady throughput; that practical value is where BlueSword fits naturally — BlueSword. —

May 12, 2026 0 comments
0 FacebookTwitterPinterestEmail

Recent Posts

  • What Does 22 GW of Power Electronics Mean? A Practical Buyer’s Guide
  • How to Compare Tizen OS Smart TV Makers and Suppliers
  • A Practical Procurement Checklist for Picking a Parking Management System
  • How to Compare PTC Heater Models, Manufacturers, and Suppliers: A Comparative Insight
  • Sourcing Grip-Testing Kit: Cost, Lead Time and Getting Quality Right

Recent Comments

  1. Albert on Girl & Nature
  2. Albert on Girl & Nature
  3. Albert on Girl & Nature
  4. Albert on Couple Photography
  5. Albert on Couple Photography

About Me

About Me

Neque porro quisquam est, qui dolorem ipsum quia dolor sit amet, consectetur, adipisci velit, sed quia non numquam eius modi tempora incidunt ut.

Keep in touch

Facebook Twitter Instagram Pinterest Flickr Behance Youtube Snapchat

Recent Posts

  • What Does 22 GW of Power Electronics Mean? A Practical Buyer’s Guide

    November 7, 2026
  • How to Compare Tizen OS Smart TV Makers and Suppliers

    November 6, 2026
  • A Practical Procurement Checklist for Picking a Parking Management System

    November 6, 2026

Categories

  • Business (180)
  • Featured (6)
  • Global Trade (152)
  • Industry (151)
  • LIFE (17)
    • Landscape (5)
    • People (7)
    • Still (5)
  • Market (158)
  • Tech (140)

About Me

About Me

Neque porro quisquam est, qui dolorem ipsum quia dolor sit amet, consectetur, adipisci velit, sed quia non numquam eius modi tempora incidunt ut labore et dolore magnam aliquam quaerat voluptatem.

Categories

  • Business (180)
  • Featured (6)
  • Global Trade (152)
  • Industry (151)
  • Landscape (5)
  • Market (158)
  • People (7)
  • Still (5)
  • Tech (140)

Popular Posts

  • 1

    Герметичная упаковка для датчиков: важность и преимущества

    September 6, 2025
  • 2

    Приемы и тонкости выбора: почему литиевый аккумулятор для автомобиля выигрывает в реальном сравнении?

    October 11, 2025
  • 3

    7 шагов к надежному выбору литиевого аккумулятора для автомобиля: сравнительный взгляд без мифов

    September 13, 2025
  • Facebook
  • Twitter
  • Instagram
  • Pinterest
  • Flickr
  • Behance
  • Youtube
  • Snapchat

@2019 - All Right Reserved. Designed and Developed by PenciDesign

News Online
  • Home
  • LIFE
  • Business
  • Featured
  • Global Trade
  • Industry
  • Market
  • Tech