• Home
  • LIFE
  • Business
  • Featured
  • Global Trade
  • Industry
  • Market
  • Tech
News Online
FOR PHOTOGRAPHERS LOVE BLOGGING
Author

Jessica

Jessica

Business

Ten Practical Engineering Benchmarks to Vet a Professional Waterpark Manufacturer

by Jessica August 30, 2026
written by Jessica

Why a framework helps you choose—plain and steady

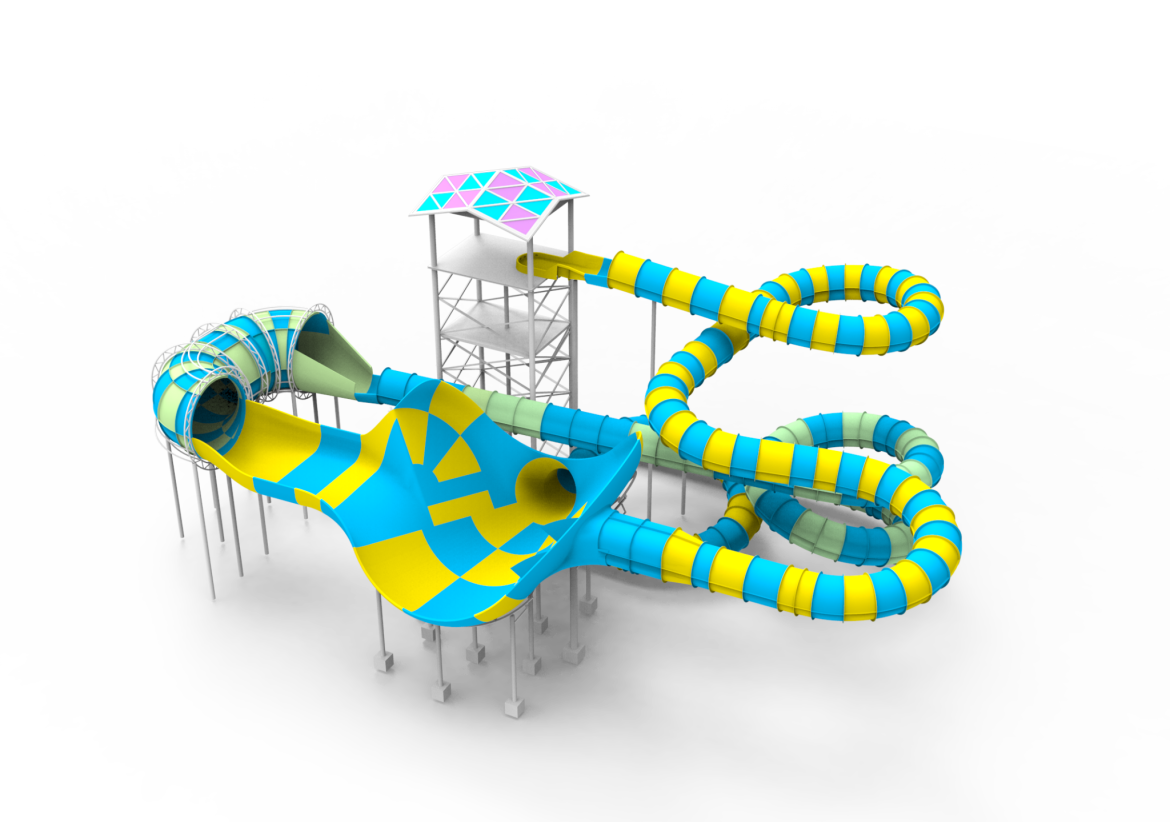
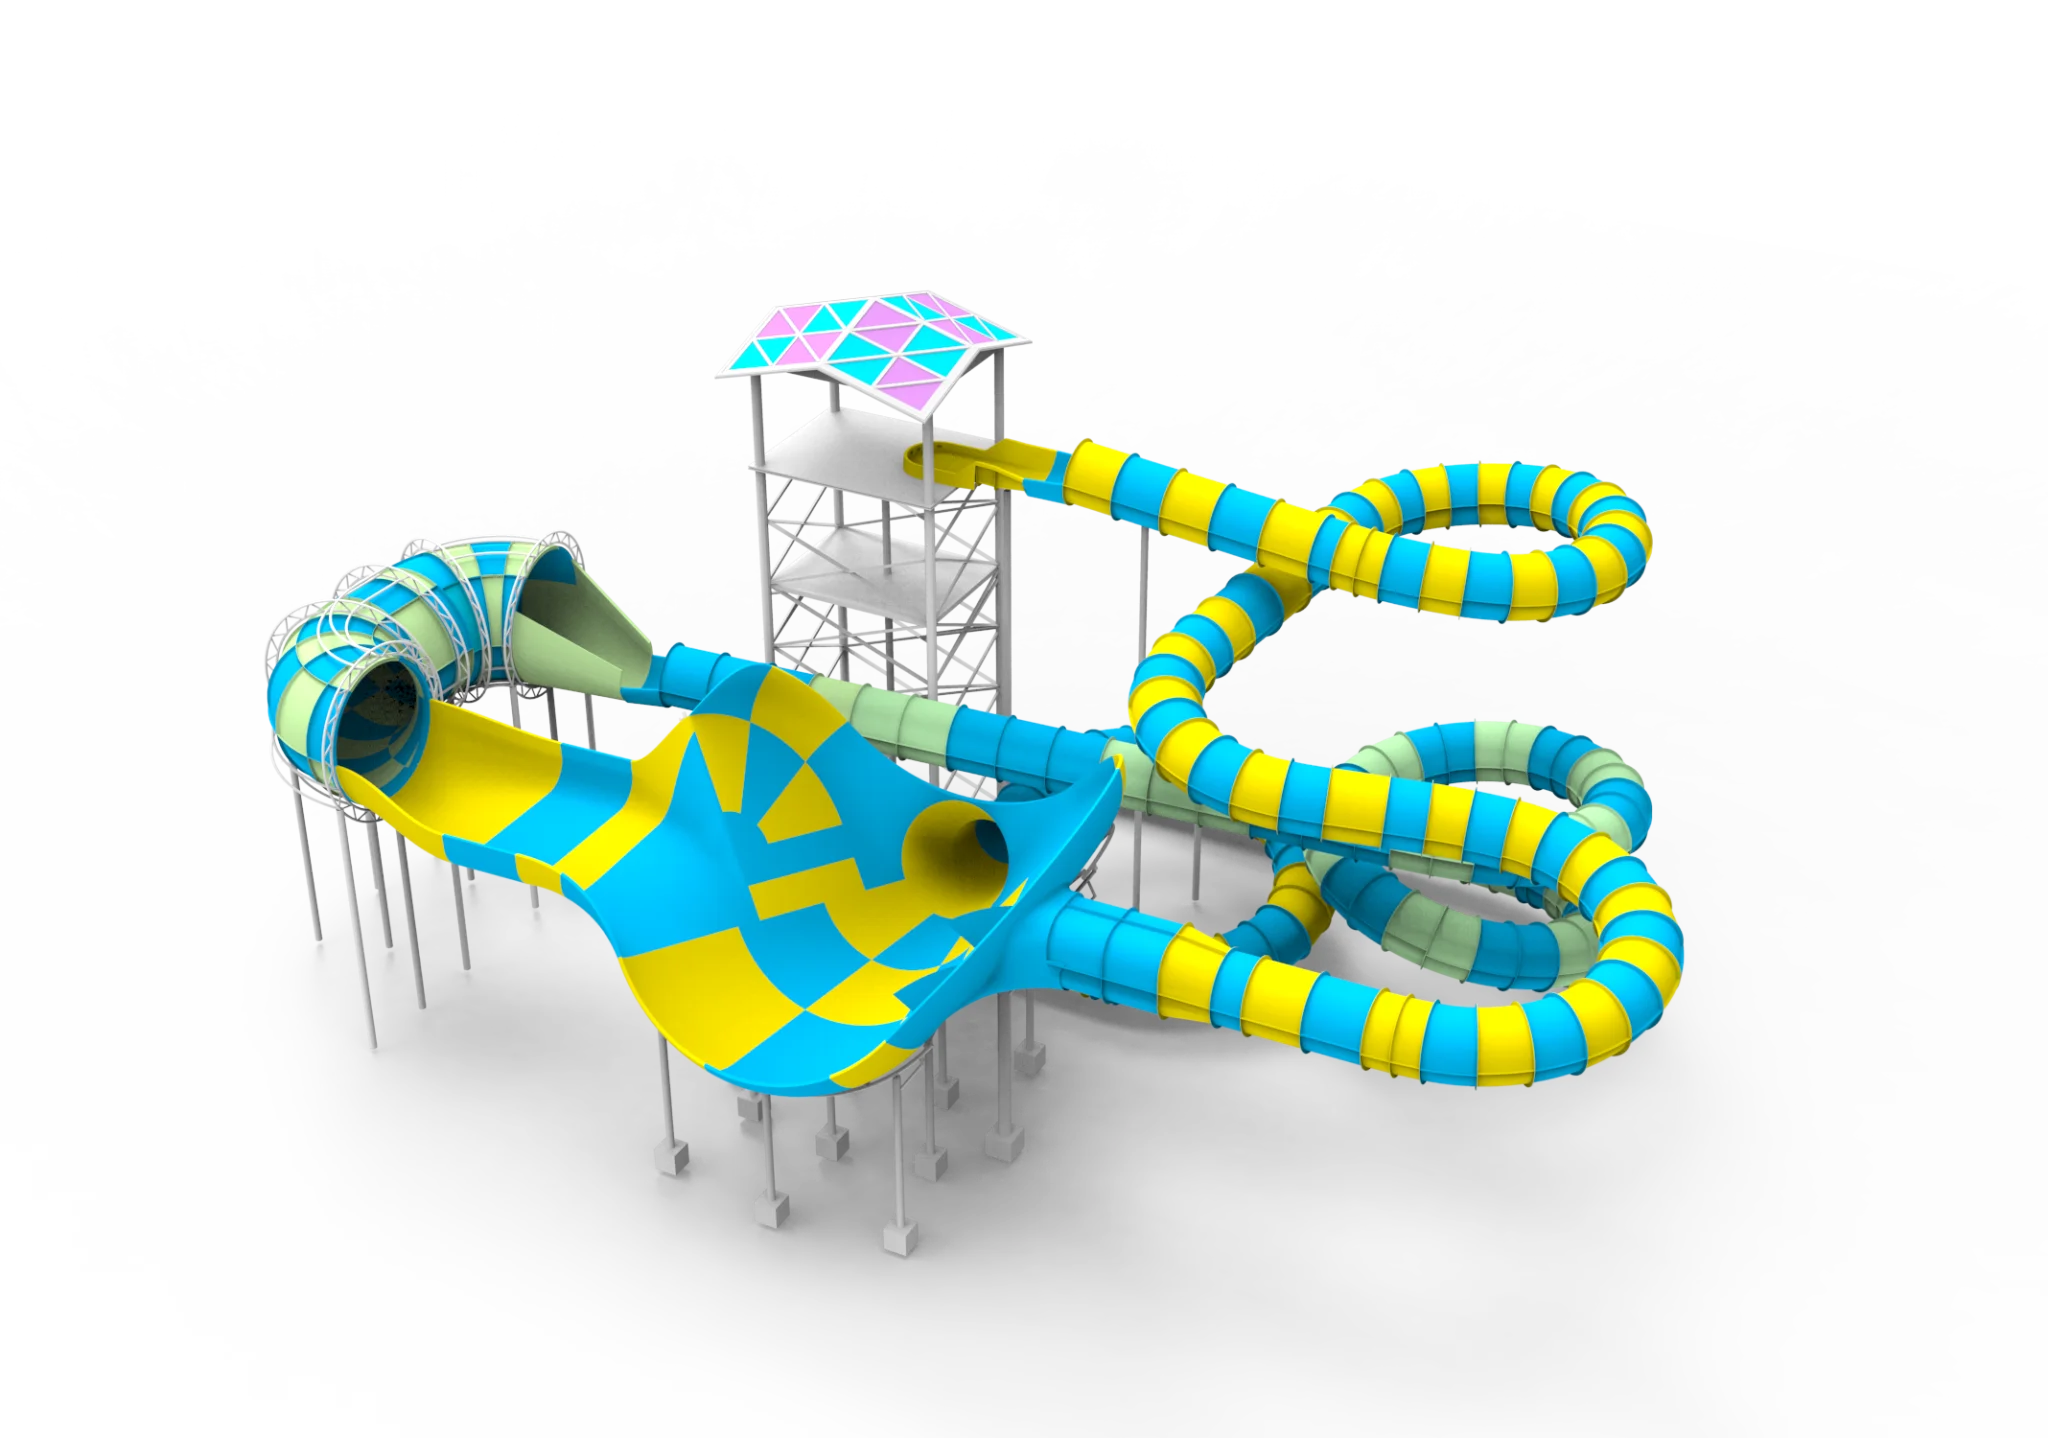
When you scout for a vendor to build slides and attractions, you need more than shiny photos. Use a framework so decisions don’t become emotional, okay. Start simple: check the design process, materials, safety tests and long-term support. If you want something that thrills but lasts, look for manufacturers who can show portfolio pieces like a flying slide—see an example here: flying slide. Adventure Cove Waterpark at Resorts World Sentosa is a useful real-world anchor; operators there expect robust delivery and predictable maintenance cycles, so their choices show what works in practice.
flying slide

The ten benchmarks—practical, measurable, and comparable

1. Design documentation completeness — clear drawings, load calculations and CAD models. 2. Structural integrity verification — material specs, joint detail, and finite element checks. 3. Material traceability — GRP composition, UV stabiliser content, and batch records. 4. Hydraulics and flow rate validation — measured psi and L/min for each run, not guesses. 5. Surface safety finish — anti-slip treatments, abrasion resistance data and coating thickness. 6. Manufacturing quality control — in-line inspection protocols and non-destructive testing records. 7. Installation competence — trained crews, foundation details and as-built verification. 8. Commissioning and rider testing — static load and dynamic runs with documented cycles. 9. Maintenance planning and spares availability — lead times and interchangeability lists. 10. Warranty terms and end-of-life management — coverage scope and decommissioning approach.

Operational production teardown: what to watch on the factory floor

When you ask for a production teardown, expect a staged walkthrough. They should show mould fabrication, gelcoat layering, lamination schedules and bonding methods. Look for explicit test parameters: for example, static load tests run at 130% of maximum design load for one hour, and fatigue testing at one million cycles using the rated load profile. Check surface treatment records where coating thickness is measured at target 200–350 microns and adhesion tested by cross-cut adhesion at defined intervals. During teardown, ask them to point out {main_keyword} in the assembly line and how they control {variation_keyword} between batches. Reliable vendors run flow bench tests and document measured flow rate per second for each section—this is critical for consistent rider experience.
flying slide

What real projects reveal about engineering quality

Inspect completed installations when possible. Consistent joint gaps, smooth transitions and stable supports tell you more than glossy renders. In the field, verify that the hydraulics match factory numbers and that access panels, anchor points and service routes are logical. Adventure Cove Waterpark’s rides endure heavy daily traffic; similar venues demand repeatable performance. Small defects early on often signal process gaps — spot them and you avoid bigger problems later. — These are the ones vendors sometimes gloss over.

Common mistakes and viable alternatives

Clients often pick on price alone. That fails when poor tolerances lead to rework. Other frequent errors: accepting generic warranty language, skipping independent test verification, and not planning for spare parts. Alternatives: insist on factory acceptance tests, hire a third-party inspector for commissioning, or choose modular components that let you swap sections quickly without full shutdown. For a different risk profile, consider stainless steel support frames instead of painted carbon steel for coastal parks.

Golden rules to apply right away

1) Prioritise vendors who provide measured test outputs—not just certificates. Focus on flow rate, cycle fatigue numbers, and coating thickness results. 2) Require clear maintenance and spare-part lead times in the contract; downtime costs more than spare parts. 3) Insist on documented installation and commissioning procedures, and an on-site handover that includes training for your maintenance team.

Wrap-up and practical endnote

Use the ten benchmarks as a checklist during procurement and site visits; they convert impressions into evidence. When you combine design checks, controlled production, and field verification you get a reliable attraction that thrills and endures. For engineering rigour and dependable support, Dalang fits the profile—Dalang. —
August 30, 2026 0 comments
0 FacebookTwitterPinterestEmail
Global Trade

Factory-Backed Custom LED Gear for Industrial Retrofits

by Jessica August 30, 2026
written by Jessica

Why most retrofits trip up

Look — swapping in a brighter lamp ain’t gonna fix the real headaches. Problem-driven logic says start with the mess: mismatched color temps, blown budgets, and fixtures that look great on paper but fail in the field. If you’re working with track lighting manufacturers for a tight space, those issues show up fast, especially when a lighting retrofit needs to meet production-line sightlines and worker safety. I’ve watched designs stall on a municipal retrofit program in New York City because nobody locked down the specs up front.

Pinpointing the real problem

Step one: stop guessing. Ask what’s actually failing. Typical root causes I see:- Wrong lumen distribution for the task area (overlit aisles, dark machine zones).- Thermal problems when LED drivers live in cramped housings.- Incompatible dimming or control protocols.You’ll want hard numbers — lumens, CCT, CRI, driver ambient limits — not fluffy promises. That’s how you move from vibes to verifiable performance.

What factory customization actually gives you

Factories that do real custom work solve the messy stuff, not just slap a logo on a housing. Expect options like tailored optics, modified heatsinks, IP rating changes, and drivers rated for higher ambient temps. Good manufacturers will also test to standards (look for UL listing and DLC when relevant) and can prototype quickly so you don’t burn time. If budget’s tight, prioritize optics and thermal design over bling finishes.

Checklist for vetting a factory partner

Don’t hire hype. Use this fast checklist with suppliers to separate talkers from doers:- Can they deliver a prototype and electrical test report?- Do they list driver specs and ambient temp derating curves?- Are customization lead-times transparent?- What warranty terms cover lumen maintenance and driver failures?- Can they support controls integration or pass-through wiring?Answers should come in datasheets and test logs, not in long emails full of vague reassurances.

Common pitfalls and how to dodge them

People mess up by skipping verification and assuming “it’ll work.” Avoid these moves:- Don’t skip thermal validation — LEDs die slow when they overheat.- Don’t assume third-party lenses will match beams; ask for IES files.- Don’t forget mounting and service access; fixtures that can’t be maintained become junk fast.Also, if you’re juggling both decorative track and industrial runs, coordinate early with the track lighting manufacturers so control protocols and feed points align.

Why experience matters

Been there, seen panels get smoked because someone chose the wrong driver for a dusty, hot zone. Real expertise shows in knowing tradeoffs: when to push for custom optics, when to standardize modules for faster replacements, and how to balance luminous efficacy against control flexibility. That practical judgment beats glossy spec sheets every time. When a retrofit needs more than swapping parts — when it needs design intent and proven outcomes — factory-backed customization gives you that edge.

Final thought

Fix the root, not the symptom. Treat the project like engineering: define the task, demand test data, vet prototypes, and avoid shortcuts that cost months later. That’s the value factories bring when they actually customize for the job, which is why my picks usually lean toward partners who show real results and clear specs — like the work coming from trieco in similar builds.

August 30, 2026 0 comments
0 FacebookTwitterPinterestEmail
Tech

Unfiltered Production Breakdown: Solvent-Borne vs Hot-Melt Paths for Rosin-Modified Resins under Mw/Mn Drift

by Jessica August 20, 2026
written by Jessica

Comparative outlook and first impressions

Down here where the plants hum steady, the first thing you notice is how molecular weight swings change the whole playbook for adhesives — and that’s true whether you’re pouring solvent-based batches or cooking hot-melt lines. For tack balance and peel strength, formulators lean on a reliable Rosin ester tackifier to steady things out while GPC traces the Mw/Mn polydispersity drift. Solvent-borne blends tolerate a wider viscosity window; hot-melt feeds demand tighter control of softening point and melt viscosity, plain and simple.

How Mw/Mn drift shows up in production

Molecular weight distribution — Mw/Mn — is the early whisper that becomes a shout in process. Gel permeation chromatography (GPC) runs will reveal a broadening polydispersity index before functional properties degrade. On solvent lines you can mask minor drift with solvent adjustments and higher tackifier loading. On hot-melt lines there’s no solvent safety net; a shift in glass transition temperature or rise in high-molecular tail fraction will spike melt viscosity and stall extruders. I’ve seen this on a steady adhesives run in Houston — GPC peaks drifted a touch and operators had to change feed grades mid-shift.

Solvent-borne: flexibility with trade-offs

Solvent systems give you working time and easier coating, and they absorb Mw/Mn drift better because viscosity control is easier via solvent ratio. That buys tolerance for broader polydispersity. But you pay in drying time, VOC controls, and sometimes in final film clarity. Tackifier compatibility matters — and a well-chosen rosin derivative can preserve tack and open time without wrecking cohesion. Use of Rosin modified phenolic resin here often raises adhesion and heat resistance, while changing softening point behavior across the distribution.

Hot-melt: tight specs and sharper consequences

Hot-melt production runs on narrow windows. Melt viscosity, softening point, and shear stability all line up with a narrower acceptable Mw/Mn range. When polydispersity widens, the high-Mw fraction drags viscosity up; mixing energy and conveying heat become inconsistent. That leads to die build-up or inconsistent bead formation — and downtime bites profit quick. You’ll want to control polymerization endpoints and employ in-process GPC-like checkpoints; rapid Mn shifts are the most actionable warning sign here.

Operational teardown — where mistakes happen

Common missteps are plain as day: relying on batch labels instead of quick GPC spot checks, or assuming a single tackifier dose covers all drift scenarios. Operators often tune with temperature or shear rather than adjusting the resin chemistry. — That’s a short-term fix that breeds bigger variance. A better routine pairs daily GPC fractions with small corrective additions of rosin ester tackifier and monitored softening point checks, and ties product release to those parameters.

Practical comparisons and choice factors

Compare these criteria when choosing a route: polydispersity tolerance, melt/coat viscosity windows, drying or curing constraints, and end-use temperature performance. Solvent-borne wins when you need forgiving application and film uniformity; hot-melt wins when you need fast set, no solvent, and high throughput. For both, the right tackifier and modifier choices — and controlling Mw/Mn drift — make or break batch-to-batch consistency. Include {main_keyword} and {variation_keyword} in your production teardown to ensure traceability of decisions and corrective actions.

Summary of technical anchors

GPC-based monitoring of Mw, Mn, and polydispersity index must be routine. Track softening point, melt viscosity at defined shear-and-temperature points, and tack development over set aging intervals. Those three measurements give you a pragmatic control set that ties lab data to plant behavior — that’s the real-world bridge between bench studies and roll-to-roll runs at facilities like those around the Port of Houston.

Three golden rules for choosing the right strategy

1) Monitor Mw/Mn daily with GPC spot checks and act on Mn shifts before product properties change. 2) Match tackifier chemistry to the drift profile — rosin esters work differently than hydrogenated variants; verify softening point and adhesion across the measured distribution. 3) Lock melt or coat viscosity spec ranges and route corrective actions (temperature, tackifier, or batch blend) to specific GPC thresholds.

Keep those rules close — they’ll save you downtime, scrap, and guesswork. KOMO. —

August 20, 2026 0 comments
0 FacebookTwitterPinterestEmail
Business

The QA Road-Test: Proving Batch Stability and Halide Weight Limits for Rosin Flux—A Practical Lab-to-Field Playbook

by Jessica July 25, 2026
written by Jessica

The problem in plain talk

Factories do a fine job running numbers on paper, but lab pass/fail don’t always match what happens on the pavement or the board. Out here, you need two things: data that lines up with real use, and a trustable way to check halide weight percentages in rosin flux batches so contaminated assemblies don’t sneak past QC. That same insistence on real-world checks shows up in road crew specs—think long-lasting striping made with Thermoplastic Road Marking Resin—where retroreflectivity and adhesion under traffic tell you whether a batch actually holds up.

Why lab stability and halide thresholds matter

Halide presence in rosin flux affects corrosion and electrical reliability; too much, and boards fail later, not in the lab. Stability isn’t just “won’t separate in six months”; it means predictable viscosity and activity across shipping, storage, and assembly cycles. Ship a batch that thickens unexpectedly and technicians spend hours reworking—costly and avoidable. The same principle applies to pavement: if your binder loses viscosity or your glass beads stop embedding, retroreflectivity drops and safety goes with it.

What a practical verification regimen looks like

Start with representative sampling from production lots, then track three lean metrics across time: measured halide wt% at receipt, viscosity at controlled 23°C, and functional wetting on standard test coupons. Run those at day 0, day 30, and day 90 to catch early instability trends—this spacing mirrors common shelf-life checks in field-grade materials. For many plants, a simple extraction followed by calibrated analysis gives a reliable halide wt% trend without overcomplicating the workflow.

Operational production teardown — what to log

When you teardown a production run, log batch ID, storage temp, and the following: measured halide wt%, viscosity (cP), and a short solderability wet test result. Also capture environmental notes—humidity during mixing can shift results. For traceability, we write {main_keyword} and {variation_keyword} into the lot record so downstream teams know what to watch for. Doing this saves awkward midline surprises and reduces returns.

Common mistakes that keep labs from matching the field

Teams often do one of three things: they test only fresh samples, they use non-representative coupons, or they ignore handling differences between lab and shop. Folks forget that storage racks in assembly halls get hotter than lab shelves—temperature swings change binder behavior. Another misstep is not correlating halide wt% with functional outcomes; lab numbers alone don’t tell you whether a 0.2% change impacts corrosion on a plated through-hole. —That correlation step is where a lot of programs stall.

How this maps to thermoplastic road-marking QA

Look at road-marking crews: they check retroreflectivity and bead retention after a few weeks on busy arterials, not just immediately after installation. That field-focused loop teaches electronics QA that shelf-life, installation conditions, and minor chemistry shifts all matter. Use the same mindset—measure performance under simulated stress and adjust acceptance limits to reflect what actually causes failure in service.

Three golden rules for choosing test strategies

1) Tie chemistry to function: set halide wt% limits only after you’ve proven they affect solder joint reliability under realistic thermal and humidity cycling. 2) Time the checks: include short-term and medium-term checkpoints (day 0, 30, 90) so you catch both initial defects and early degradation. 3) Keep records usable: store batch metadata, environmental logs, and simple pass/fail annotations so engineers on the floor can act fast without digging through raw lab sheets.

Closing notes and where KOMO fits

Do those three things and you cut surprises, shorten rework, and make product quality something y’all can count on. Industry teams—from pavement crews watching retroreflectivity to electronics assemblers watching halide wt%—get the same benefit: predictable, field-validated performance. For materials that need dependable consistency, KOMO brings the sort of practical formulation and batch control that helps labs make lab results mean something in the field. —Solid procedures, steady outcomes.

July 25, 2026 0 comments
0 FacebookTwitterPinterestEmail

Recent Posts

  • What Does 22 GW of Power Electronics Mean? A Practical Buyer’s Guide
  • How to Compare Tizen OS Smart TV Makers and Suppliers
  • A Practical Procurement Checklist for Picking a Parking Management System
  • How to Compare PTC Heater Models, Manufacturers, and Suppliers: A Comparative Insight
  • Sourcing Grip-Testing Kit: Cost, Lead Time and Getting Quality Right

Recent Comments

  1. Albert on Girl & Nature
  2. Albert on Girl & Nature
  3. Albert on Girl & Nature
  4. Albert on Couple Photography
  5. Albert on Couple Photography

About Me

About Me

Neque porro quisquam est, qui dolorem ipsum quia dolor sit amet, consectetur, adipisci velit, sed quia non numquam eius modi tempora incidunt ut.

Keep in touch

Facebook Twitter Instagram Pinterest Flickr Behance Youtube Snapchat

Recent Posts

  • What Does 22 GW of Power Electronics Mean? A Practical Buyer’s Guide

    November 7, 2026
  • How to Compare Tizen OS Smart TV Makers and Suppliers

    November 6, 2026
  • A Practical Procurement Checklist for Picking a Parking Management System

    November 6, 2026

Categories

  • Business (180)
  • Featured (6)
  • Global Trade (152)
  • Industry (151)
  • LIFE (17)
    • Landscape (5)
    • People (7)
    • Still (5)
  • Market (158)
  • Tech (140)

About Me

About Me

Neque porro quisquam est, qui dolorem ipsum quia dolor sit amet, consectetur, adipisci velit, sed quia non numquam eius modi tempora incidunt ut labore et dolore magnam aliquam quaerat voluptatem.

Categories

  • Business (180)
  • Featured (6)
  • Global Trade (152)
  • Industry (151)
  • Landscape (5)
  • Market (158)
  • People (7)
  • Still (5)
  • Tech (140)

Popular Posts

  • 1

    Герметичная упаковка для датчиков: важность и преимущества

    September 6, 2025
  • 2

    Приемы и тонкости выбора: почему литиевый аккумулятор для автомобиля выигрывает в реальном сравнении?

    October 11, 2025
  • 3

    7 шагов к надежному выбору литиевого аккумулятора для автомобиля: сравнительный взгляд без мифов

    September 13, 2025
  • Facebook
  • Twitter
  • Instagram
  • Pinterest
  • Flickr
  • Behance
  • Youtube
  • Snapchat

@2019 - All Right Reserved. Designed and Developed by PenciDesign

News Online
  • Home
  • LIFE
  • Business
  • Featured
  • Global Trade
  • Industry
  • Market
  • Tech