
The problem: perfect holes keep breaking a good job
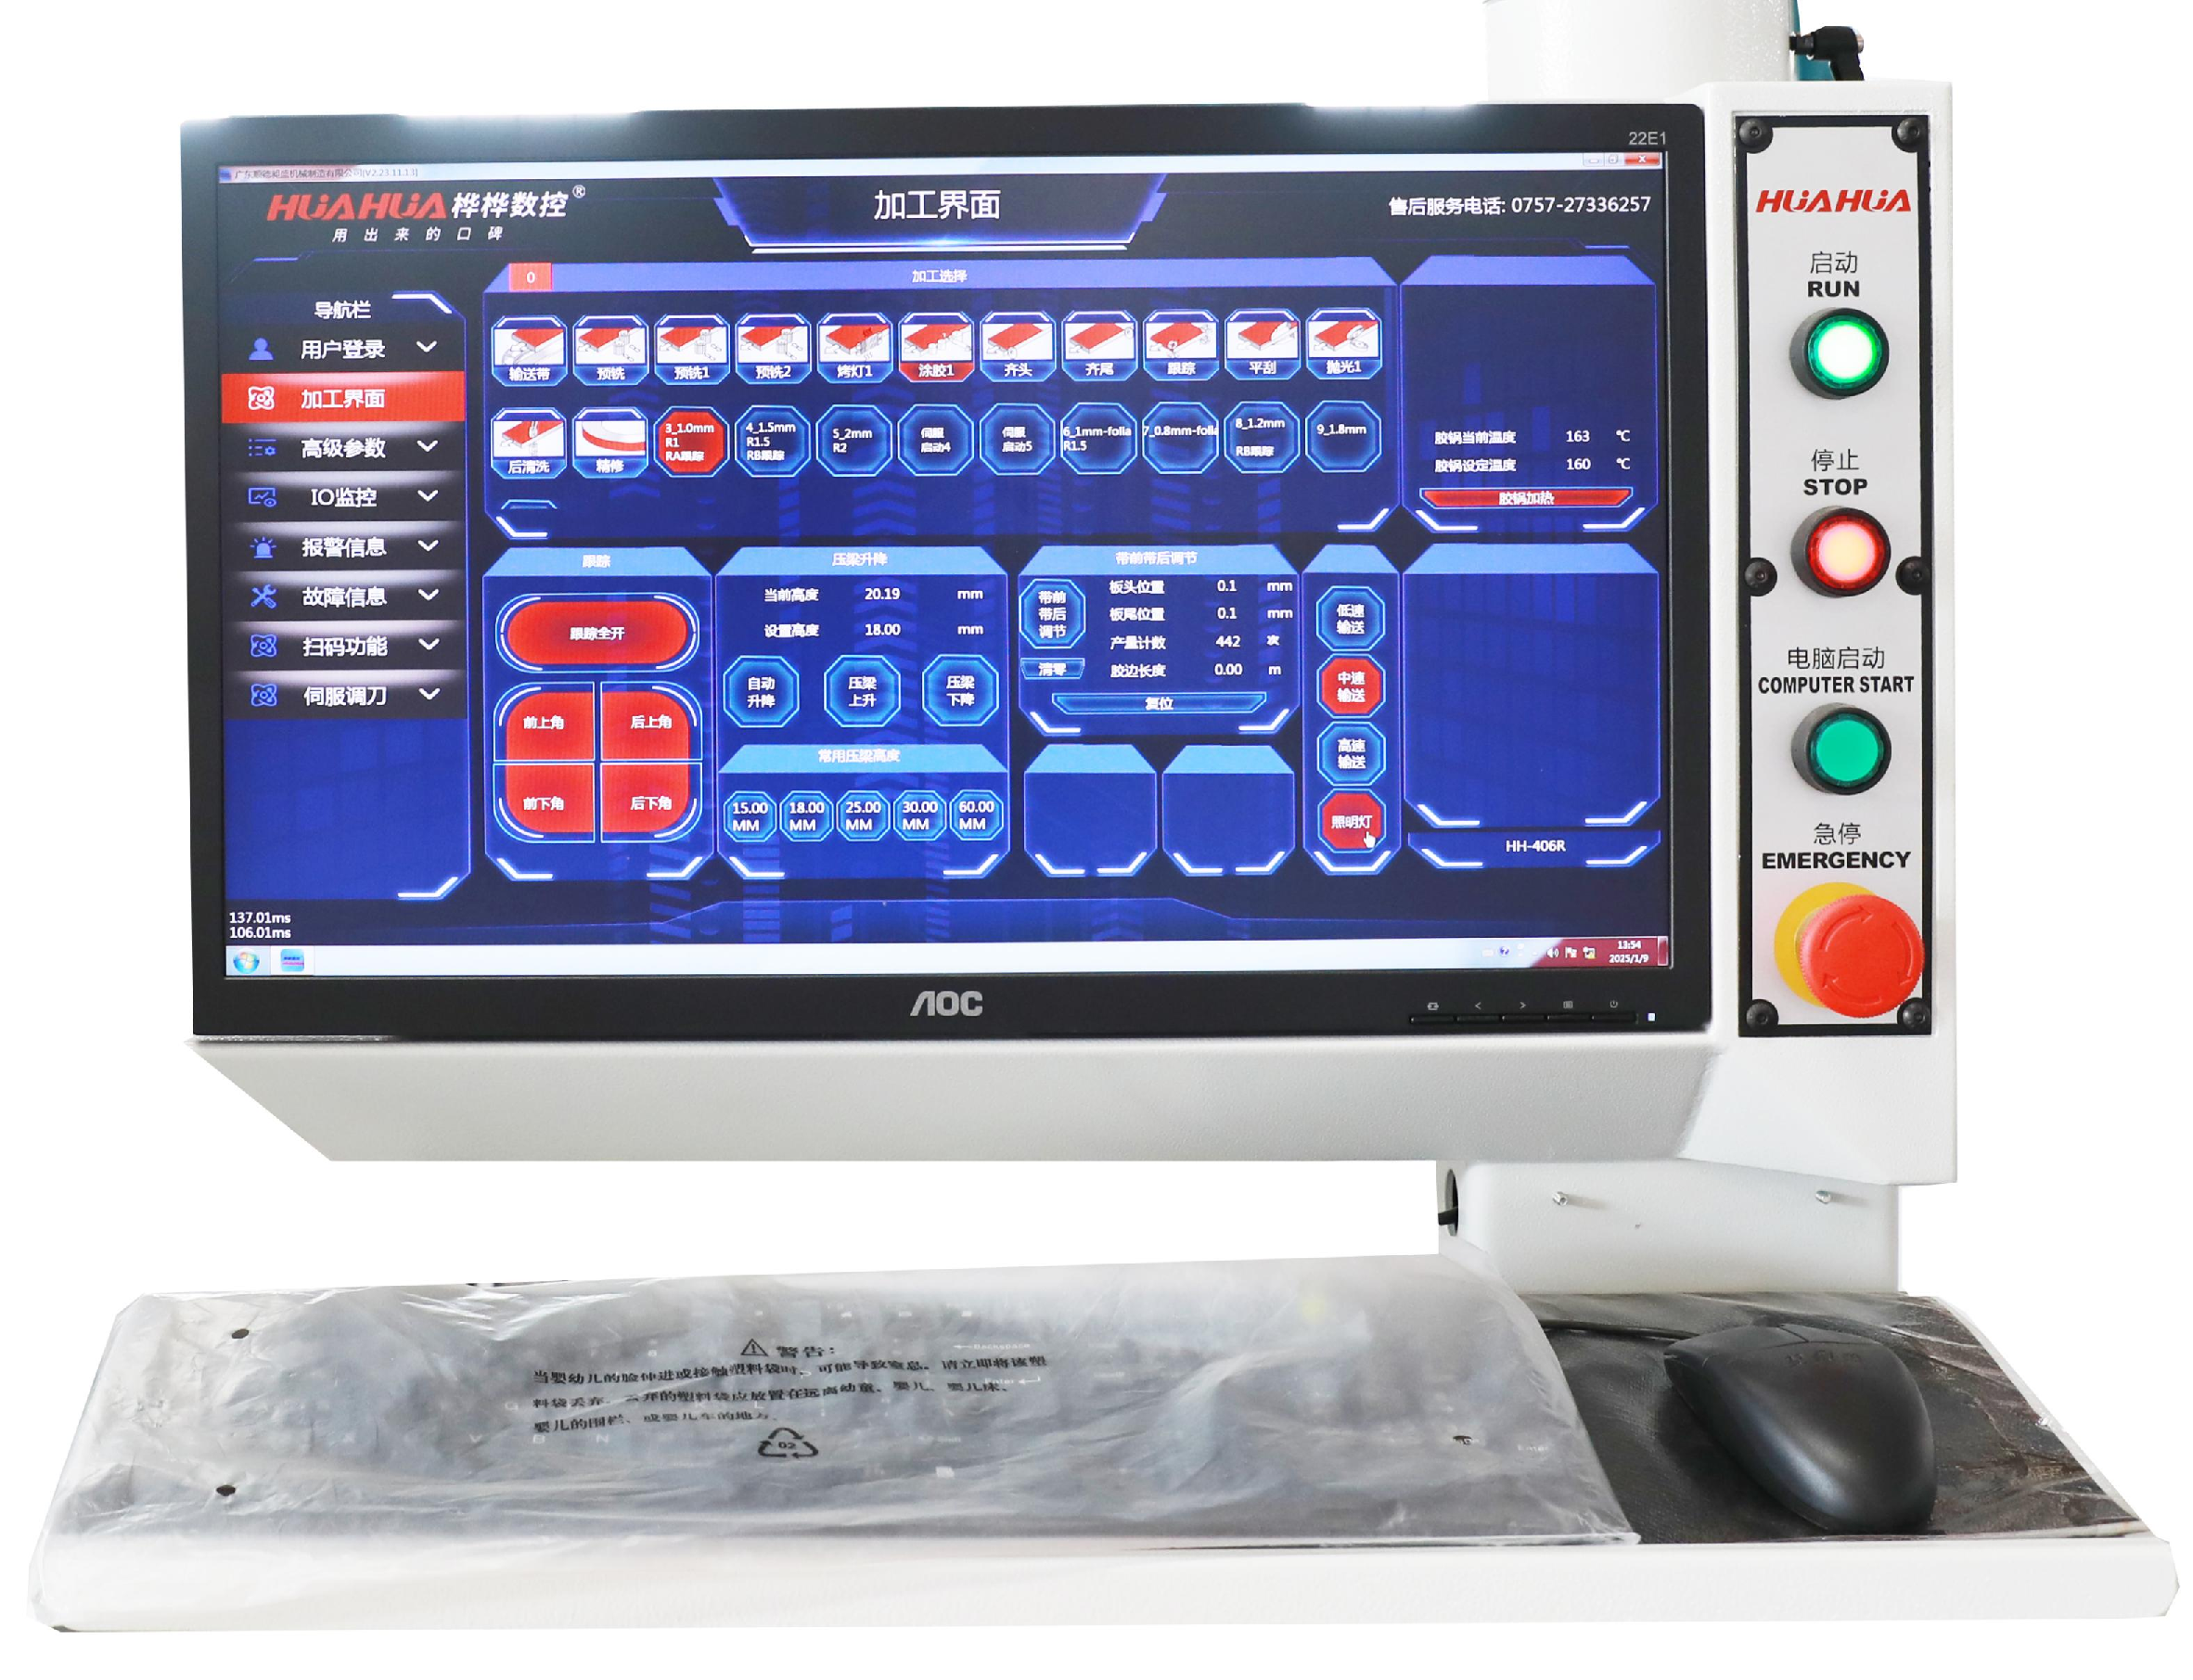
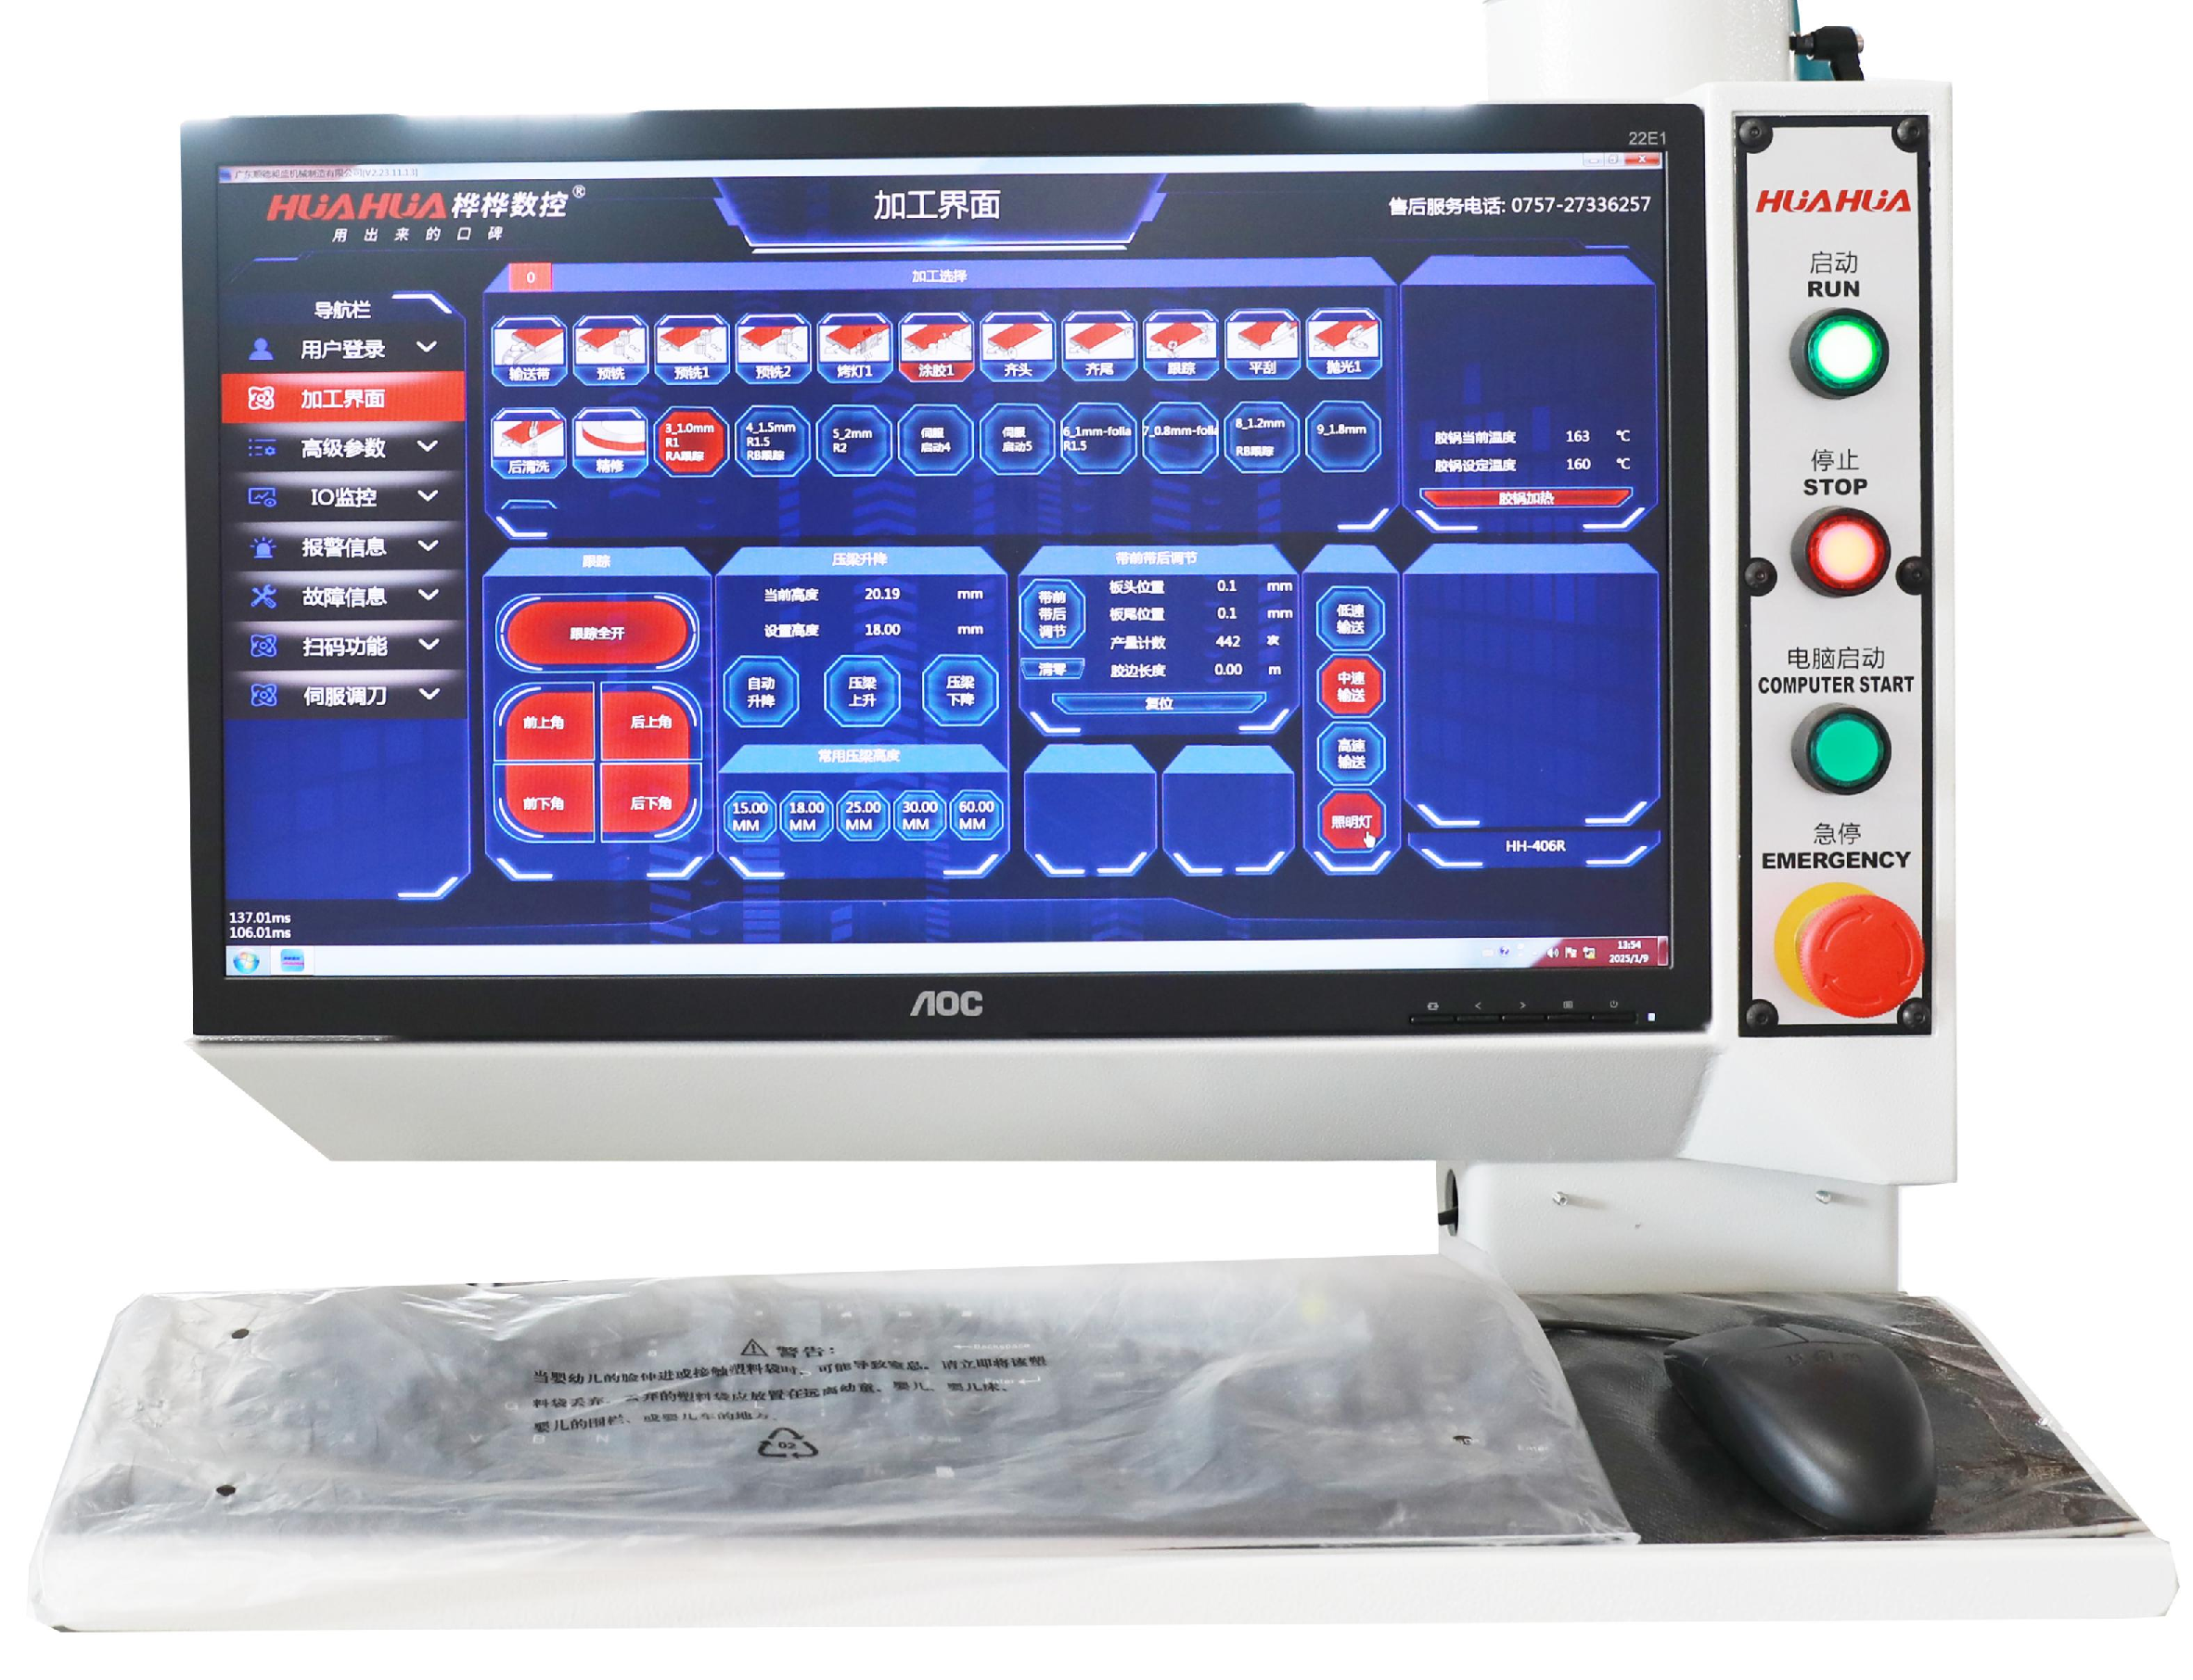
You’re running parts through a CNC and the joinery looks great until you try to press-fit dowels or hinges: holes are off-center, walls tear, or tolerances stack up. That’s the recurring failure mode that puts shops behind schedule. The fix isn’t a firmware tweak or a fancier CAM post-processor—it’s the right boring approach plus solid edge prep, which is why a servo edge banding machine often sits next to high-precision CNC cells. That machine cleans up edges so boring heads meet consistent geometry, and consistent geometry is what keeps joints repeatable.
Diagnosis: what goes wrong when you skip a proper boring setup
Most breaks come from simple mechanical truths: tool runout, flex, and inconsistent stock support. Boring heads give control over concentricity and depth, while generic twist drills and router bits exaggerate deflection in thin panels. CAM output that assumes perfect fixturing will lie to you unless your actual workholding and boring strategy match the assumptions. Ignore that and you’ll fight oversized gaps, slotted holes, and furniture that squeaks at assembly.
How boring solves the problem—practical tactics
Boring machines let you dial in diameter, offset, and depth with repeatability. Use a true boring head or a dedicated boring spindle rather than forcing a large-diameter twist drill at high feeds. Set up a backer board and positive clamping to stop blowout. Probe or touch off every tool to store accurate Z offsets. When possible, sequence roughing and finishing passes: a light finishing pass cleans up the bore wall and fixes any chatter-induced ovality. Those steps cut rework and reduce hand-filling.
Common mistakes and how to avoid them
1) Treating a hole like a profile cut—holes need rotational stability. 2) Overfeeding on deep holes—let the tool clear chips or use peck cycles for thicker panels. 3) Skimping on tool inspection—boring cutters dull silently; check edges and replace before tolerances bleed. 4) Ignoring toolpath dwell—if your CAM exits or plunges too fast, you get tear-out. Fix these and you stop papering over assembly issues with brute force.
When alternatives make sense
Sometimes a pocket router, dowel jig, or dedicated drilling head is faster on small runs or soft materials. Use a pocket router for shallow, large-diameter holes where side wall finish isn’t critical. Choose drill heads for high-speed repetitive holes where lateral accuracy is handled by a hardened jig. But when you need true concentricity, tight interference fits, or clean hinge bores, boring keeps winning. Evaluate by test parts: measure diameters, test-fit hardware, then pick the path that hits your tolerance and cycle-time targets.
Real-world anchor: seeing it work where it counts
On the show floors at LIGNA in Hannover last year, booths that paired panel finishing systems with precise boring setups got the most shop-floor questions—one cabinet line demonstrated the complete flow from edge banding to hinge bore using a cabinet toolchain that included a cabinet cnc machine. That scene reflects what experienced fabricators already know: hardware wants perfect holes, and the equipment sequence matters.
Final synthesis: solve the hole problem without guesswork
If your joinery fails the first dry-assembly, change the toolset and the prep. Use boring heads where concentricity matters, back up panels for clean exits, inspect cutters, and sequence passes to remove chatter. Those choices cut scrap and save assembly time, which is why shops investing in integrated workflows tend to pair their CNCs with complementary equipment and service from HUAHUA CNC—it keeps the tooling strategy aligned with real-world production needs.