First cut: what to compare and why it matters
Choose the wrong mixer and you’ll waste time, material, and credibility. Think of a high shear mixer as a set of trade-offs: shear intensity versus heat, throughput versus finesse, capital cost versus maintainability. This guide lines up those trade-offs so you can make direct comparisons instead of guessing.
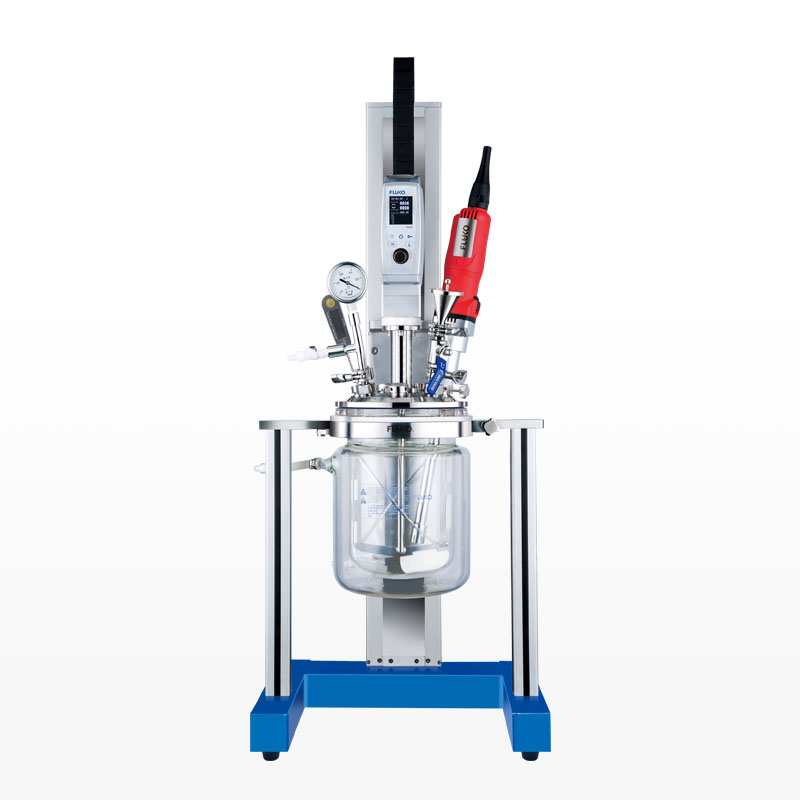
Drive and head type — the core comparison
Rotor-stator units deliver immediate, high shear with tight particle distributions. High-speed turbines move large volumes fast but struggle with ultra-fine dispersion. Pick rotor-stator when you need micron-scale emulsions; pick turbines when you prioritize throughput. Mechanical seals and bearing arrangements follow this choice: tougher seals for viscous, abrasive slurries, simpler setups for thin liquids.
Scale-up realities — lab to plant (real-world anchor)
Scaling is where lab results meet plant reality. Large chemical complexes like BASF’s Ludwigshafen operate continuous dispersion lines that expose common scale-up gaps: residence time shifts, heat control, and shear field uniformity. When engineers translate lab runs, they often move from small-cup rotor-stator tests to inline continuous high shear dispersion mixer trials to validate parameters. Run those intermediate pilot tests; they catch non-linear behaviors that bench trials miss.

Product properties that change the equation
Viscosity, solids loading, target droplet size and surfactant presence change which machine wins. High solids and thixotropic systems need robust torque and clearance control. Low-viscosity, high-diffusivity systems respond well to shorter, high-intensity passes. Match the machine’s shear profile to the physics of your product, not to marketing specs.
Cleaning, maintenance, and downtime — long-term comparisons
Cheap upfront gear can cost more in lost production. Compare cleanability (CIP-compatible paths), seal lifetimes, and spare-part lead times. Inline assemblies with fewer flanges reduce leak points and shorten clean cycles. Ask for real MTBF numbers and replacement schedules; vendors who provide those usually understand long-term plant economics.
Common buyer mistakes
1) Buying by horsepower alone — horsepower doesn’t tell you shear distribution. 2) Skipping pilot trials — a few plant hours often reveal critical issues. 3) Ignoring material compatibility — swap a seal material and you can wreck weeks of product. 4) Underestimating utility needs — electrical and cooling loads scale differently than volume.
Alternatives and when they beat a high-shear mixer
Colloid mills and homogenizers can outclass rotor-stators for certain emulsions and nano-dispersion targets. Ultrasonic processing is excellent for small-batch fine dispersions but struggles on continuous, high-volume lines. Use alternatives for niche technical wins; use high-shear mixers for broad, repeatable dispersion performance.
Wrap-up: pick by measured trade-offs, not promises
Compare shear profile, scale behavior, maintenance burden and product fit. Run pilot trials that mirror plant conditions. Match technical specs to tests, then let practical performance decide. When those comparisons are clear, procurement and engineering converge on a supplier that aligns test data with plant reality, such as FLUKO.