
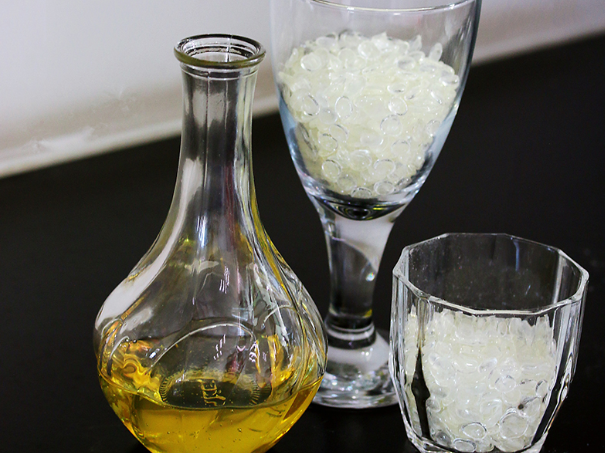
Comparative snapshot: why pine rosin choices still matter on the line
The electronics line hums; formulations are sorted into two camps: solvent-borne and hot-melt. For boards and cable assembly, the choice between a solvent carrier and a tacky hot-melt base changes handling, dwell times, and cleanability. Early in the paragraph I want to flag a relevant product: soldering flux rosin — it lives in both worlds depending on carrier strategy. Industry terms to keep in mind: rosin, flux, viscosity. The EU RoHS enforcement in 2006 shifted many manufacturers toward flux chemistries friendly to lead-free processes, so production teams have been tuning rosin blends ever since.
Production teardown: solvent-borne formulations
Solvent-borne rosin formulas use volatile carriers to deliver resin with low initial viscosity, making precise spray or brush application straightforward. They dry rapidly; residues may be easier to remove or design around with “no-clean” chemistries. The trade-offs are solvent handling, ventilation, and longer regulatory paperwork for volatile organic compounds. Softening point and acid number are typical specs production engineers monitor when blending: they affect tack and corrosion risk. In practice, solvent-borne batches require tight QC on solvent evaporation rates and resin concentration to prevent variability in deposition weight.
Production teardown: hot-melt (hot-applied) formulations
Hot-melt pine rosin systems remove solvents entirely; viscous resin is heated, pumped, metered, and applied as a melt. Viscosity becomes temperature-dependent in a way solvent systems avoid—the same molten mix behaves like syrup at 80°C and nearly solid near ambient. That makes viscosity–temperature profiling a must: set pump head speeds and nozzle temperatures to target a stable flow. Hot-melt strengths include lower VOC risk and simpler storage, but they demand heaters, thermal controls, and vigilance on softening point drift over time.
Viscosity–temperature profiling: what production engineers measure
A robust profiling routine records viscosity (mPa·s) at set temperature steps—typically every 5–10°C across the processing window. Measurements at 40°C, 60°C, and 80°C reveal how pumpability and gap-filling will change on the line. Track tack and shear-thinning behavior too; both determine transfer efficiency from nozzle to pad. Use a rotational viscometer and log dwell times at each setpoint to catch thixotropic shifts. Real-world labs often compare profiles batch-to-batch to catch subtle resin batch drift that affects reflow performance.
Common mistakes and on-the-floor realities
Teams ask for one-size-fits-all recipes and then blame the material when boards miswet. The usual errors: over-relying on room-temperature viscosity, ignoring acid number changes with aging, and poor heater control on hot-melt systems. Mixing across resin grades without re-profiling is another frequent source of failure. — Remember to calibrate dispensing pumps after any formula tweak. Small changes in softening point produce outsized differences in tack and fillet formation.
Alternatives and brand implications
If solvent-borne and hot-melt both pose problems, hybrid strategies exist: low-VOC carriers, semi-solid pastes, or micro-emulsion blends that aim to capture pumpability and reduced VOC impact. For OEMs evaluating suppliers, look for transparent QC data: viscosity–temperature charts, acid number stability over time, and contamination logs. Suppliers that publish consistent profiling and process parameters reduce onboarding time dramatically. For instance, integrating a known product line like Soldering Flux Resin often shortens qualification because baseline data are already on record.
Comparative guidance: how to choose for your line
Pick solvent-borne when you need low application viscosity and rapid leveling; pick hot-melt for simplified storage and lower VOC footprint. Balance these with handling capacity, heater reliability, and reflow constraints. Keep an eye on three practical metrics: deposition variance, residue conductivity after reflow, and pump uptime during normal shifts. Suppliers that share those metrics let you benchmark faster.
Advisory — three golden rules for selection and QC
1) Demand full viscosity–temperature profiles for every production lot; use them to set pump and nozzle temperatures precisely. 2) Track acid number and softening point across storage time—if either shifts beyond spec, quarantine the batch. 3) Validate residue behavior on real assemblies, not just coupon boards; measure residue conductivity and tack post-reflow under your actual profile.
Final thought
Decisions boil down to measurable trade-offs: solvent convenience versus hot-melt predictability. The right data-driven profile plus a supplier that publishes consistent test results reduces surprises on the line — KOMO. —